Your Trusted Labels & Stickers Manufacturer from China!

Cable and Wire Labels Manufacturer

Custom wire identification labels engineered around cable diameter, jacket surface, print area, environment, data and delivery format.
For harnesses, panels, telecom, data centers and industrial equipment, Philiton develops label structures from sample validation to repeat production.
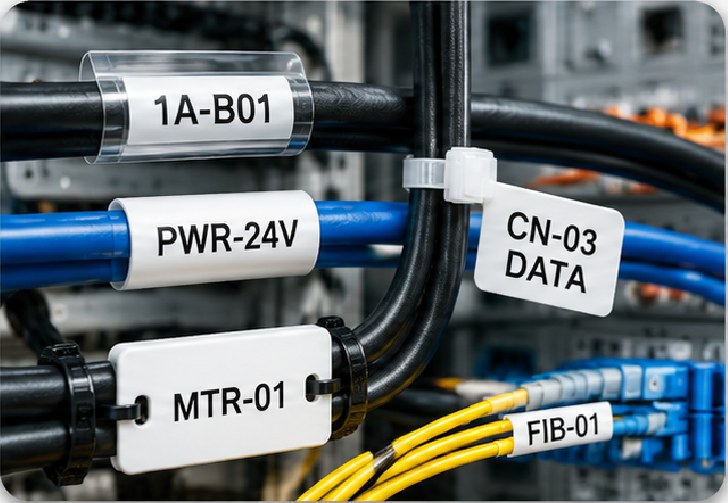
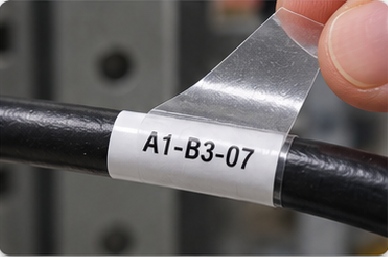
  • Self-laminating, wrap-around, wire wrap, cable flag, cable tag and network/fiber formats
  • Founded in 2016; Shenzhen + Dongguan manufacturing operations
  • 12,000+ m², 200+ employees and 91 technical, production and quality personnel
  • Many standard projects can start from around 500 pcs
Cable and Wire Labels Manufacturer

Cable Label Programs Built for Different Technical Teams

Cable identification requirements change with equipment, cable construction, installation method and data workflow. Philiton structures each project around the role responsible for performance and repeatability.

Wire Harness Manufacturers

Wire harness programs need more than readable text. Label dimensions must fit small cable diameters without excessive stiffness, variable IDs must match assembly records, and each SKU must remain separated during production and packing. Philiton reviews cable OD, jacket material, printed content, wrap direction, data source, roll format and inspection requirements before release. For repeat programs, approved artwork, material, tooling and production parameters can be retained for controlled reorders, while any change in cable, adhesive, code structure or quantity is reviewed before production.

Electrical Equipment Makers

Panel builders and electrical equipment manufacturers often manage many wire IDs across multiple machines, cabinets or product versions. Philiton can organize fixed text, sequential numbers, barcodes, QR codes and color coding into controlled artwork sets, then manufacture labels in roll, sheet or individual formats according to the assembly method. When labels feed through a printer or dispenser, core size, winding direction, pitch, liner width and maximum roll diameter become part of the specification rather than packing details added at the end.

Telecom and Data Centers

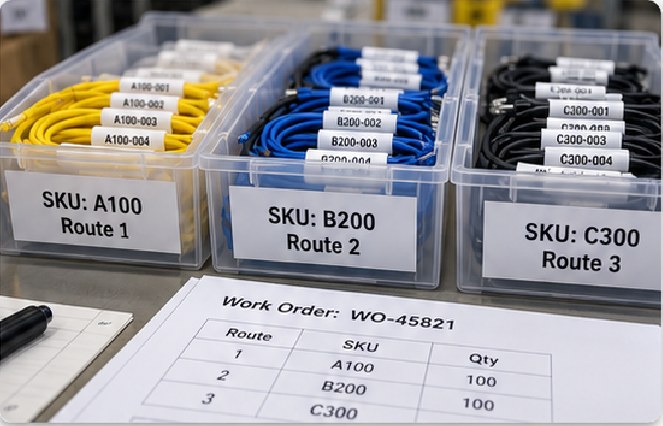
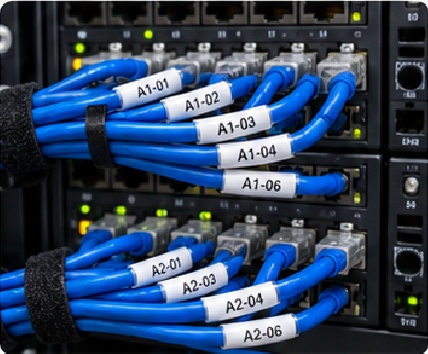
Telecom, network and data-center teams need identification that stays legible in dense cable environments where space is limited and rework is expensive. Philiton can support wrap-around, self-laminating, cable flag and tag-style identification depending on cable diameter, information area and access conditions. Projects can include port IDs, rack references, cable routes, sequential numbers, barcodes or QR codes. Multi-SKU packing can be planned by installation zone, rack, cabinet or work order so field teams receive labels in a sequence that reduces sorting during deployment.

Industrial Procurement Teams

Long-running industrial programs require stable specifications, not a one-time printed roll. Philiton links material, adhesive, artwork, die line, variable data, roll configuration, QC criteria and packing instructions into one project record. Procurement teams can start with material or printed samples, lock an approved specification, then scale into repeat production without rebuilding the project from zero. When requirements include chemical exposure, unusual temperatures, low-surface-energy jackets or compliance documentation, the exact structure is reviewed and verified before any performance claim is fixed in the production specification.

Cable and Wire Label Formats We Can Customize

Philiton supports multiple cable-identification constructions so label format can follow the cable, installation sequence, information density and service environment instead of forcing every project into one shape.
Self-Laminating Labels

Self-Laminating Labels

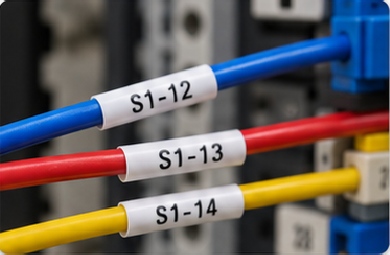
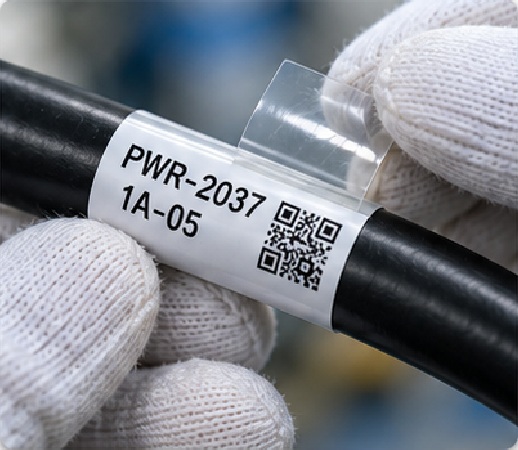
A self-laminating construction combines a printable identification area with a clear protective section that wraps over the printed field. It is useful where handling, rubbing, moisture or routine maintenance could damage exposed print. The final layout depends on cable OD, printable area, overlap and the stiffness of the selected film. Philiton can customize dimensions, colors, fixed or variable print, die-cut shape and roll configuration, then confirm fit on the actual cable before mass production.
Wrap-Around Labels

Wrap-Around Labels

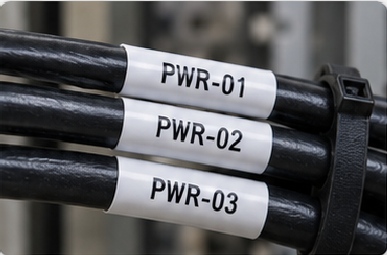
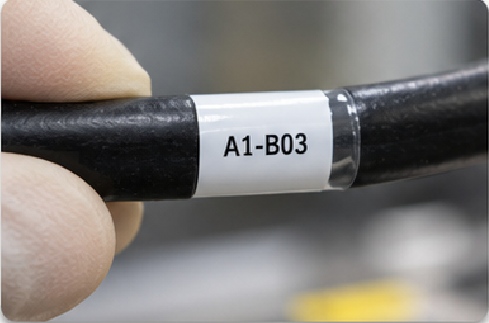
Wrap-around labels encircle a cable or wire jacket and can be produced as compact identification pieces for assemblies, panels, telecom work and industrial equipment. Cable diameter controls the minimum wrap geometry, while the amount of text or coding controls the printable zone. Philiton reviews label length, width, overlap, edge position, adhesive and liner design together so finished labels wrap cleanly without placing critical text on the overlap or creating an unnecessary lifting edge.
Wire Wrap Labels

Wire Wrap Labels

Wire wrap labels are suited to programs that need concise IDs on individual conductors or small cable groups. Common project inputs include wire OD, jacket material, ID length, character height, color coding and required roll or sheet format. Philiton can organize multiple artwork versions or sequential identifiers within one controlled production project. Small-diameter applications receive extra attention to material conformability and label stiffness because a construction that performs well on a flat panel can behave differently on a tightly curved wire.
Cable Flag Labels

Cable Flag Labels

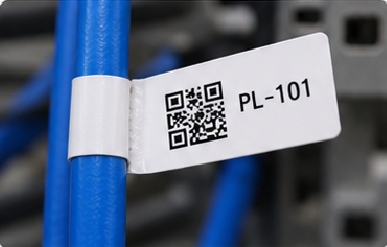
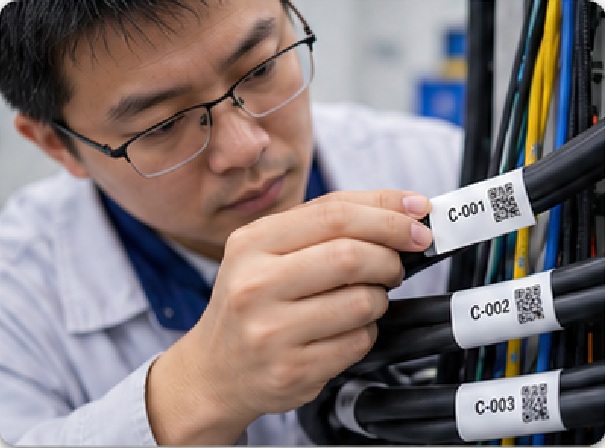
Cable flag labels create a larger readable area without requiring the full printed field to follow the cable circumference. They are useful when a small cable must carry longer text, route information, barcodes or a QR code. Philiton can adjust flag size, fold position, adhesive zone, print orientation and data layout around the actual installation method. The artwork is checked so fold lines, code quiet zones and important characters stay clear after the label is applied.
Cable Tags

Cable Tags

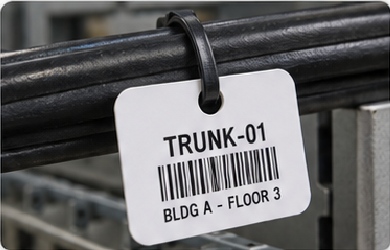
Tag-style identification is useful when direct adhesive contact is not preferred, when the cable is large, or when additional information is needed. Philiton can support printed cable tags and related identification formats using project-specified materials, hole or attachment requirements, variable numbering, barcodes and color systems. Final material and attachment method should be selected around abrasion, flexibility, outdoor exposure and service life rather than appearance alone.
Network and Fiber Labels

Network and Fiber Labels

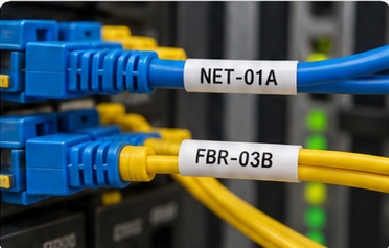
Network and fiber identification often involves high SKU counts, compact text, rack or port references and installation sequences. Philiton can produce labels with fixed fields plus changing IDs, barcodes or QR codes, and organize packing by rack, panel, zone or work order. For dense cabling, printable area and finished stiffness matter as much as print quality. Sample application on representative cable helps confirm legibility and handling before larger production quantities are released.

Select the Label Construction Before Finalizing Artwork

Cable OD, installation timing, information area and service conditions should define the construction first. Artwork becomes far easier to control once the physical identification method is settled.

Project conditionSuitable starting formatKey design inputMain risk to checkRecommended validation
Small individual wireWire wrap or self-laminating labelWire OD, character height, wrap lengthEdge lift or excessive stiffnessApply samples to actual wire and inspect after dwell
Medium cable with routine handlingSelf-laminating labelCable OD, printable zone, clear overlapPrinted field exposed to abrasionConfirm clear overwrap fully protects print
Cable needing long text or codeCable flag labelFlag size, fold line, code sizeFold hides data or code distortsScan and read after final fold
Large cable or bundleWrap-around label or cable tagBundle OD, surface, attachment methodInsufficient contact or tag movementTest on representative bundle
High-SKU harness programVariable-data wrap labelData file, sequence logic, SKU mappingDuplicate, missing or mixed identifiersData verification plus SKU-controlled packing
Network or fiber installationFlag, wrap or compact self-laminating labelPort/rack data, cable OD, install sequenceSmall text, sorting errors, reworkPilot set by rack or work order

Size Cable Labels From the Cable Outward

Cable labels should be sized from the real cable diameter and required information area, not from a standard rectangle selected before the application is known.

Use Cable OD as the First Engineering Number

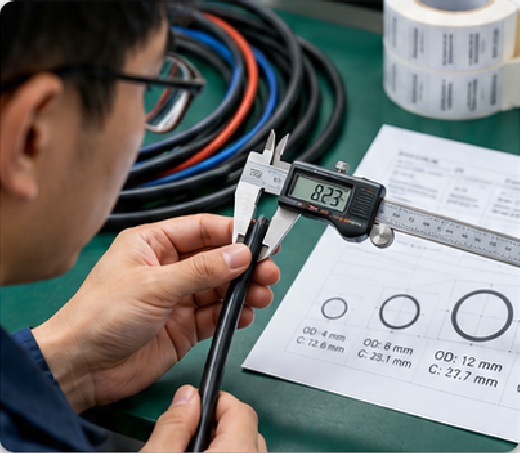
Cable outside diameter is the first dimension Philiton requests because a curved surface changes how a label behaves. Circumference can be calculated as π × cable OD: a 4 mm cable has a circumference of about 12.6 mm, an 8 mm cable about 25.1 mm, and a 12 mm cable about 37.7 mm. Those numbers do not automatically become label length; they show how much surface must be wrapped before printable area, overlap and edge position are added.

A useful sizing review separates three zones: the readable print area, the wrap or bonding area, and any protective clear overlap. Small wires usually need a more conformable construction because excessive film stiffness can pull an edge away from the jacket. Larger cables create more room for text but may introduce textured surfaces, deeper curvature transitions or larger bundles. Philiton therefore asks for actual cable OD or a physical cable sample whenever dimensions are tight.

For multi-size harnesses, one label size should not be forced across every conductor simply to reduce SKUs. A better approach is to group cable diameters into workable families, then confirm whether one construction can cover each group without sacrificing readability or adhesion. Final dimensions are approved from a dieline or printed sample before mass production.

Build Self-Laminating Labels Around the Protective Overwrap

A self-laminating label only works when printable area, clear tail, overlap and adhesive zone are designed as one construction rather than four unrelated dimensions.

Protect the Printed Field Without Hiding Critical Data

Philiton starts by defining what must remain visible after wrapping: wire ID, circuit number, barcode, QR code, warning, asset number or other controlled information. The printable field is positioned so essential text stays clear of the final overlap and remains readable from the expected viewing direction. A transparent tail can then wrap over the printed area to provide an additional protective layer against handling, rubbing and moisture.

Cable diameter determines how quickly the label curves and where the overlap lands. A clear section that is too short may leave print exposed; an unnecessarily long section adds material, increases roll diameter and can make small-wire application harder. Film flexibility, adhesive tack and liner release also affect whether the label wraps smoothly around the cable without spring-back.

For variable-data programs, the protective geometry is approved before data files are released to production. Philiton can then control text position, code size, die-cut registration, sequence and roll configuration against the approved layout. Sample labels should be applied to the actual jacket, allowed to dwell, then checked for edge lift, print coverage, scan performance and handling before bulk production. The result is a repeatable manufacturing specification rather than a visual sample alone.
Cable Identification for Real Installation Environments

Philiton develops cable labels around the conditions technicians, assemblers and maintenance teams actually face after the roll leaves the factory.
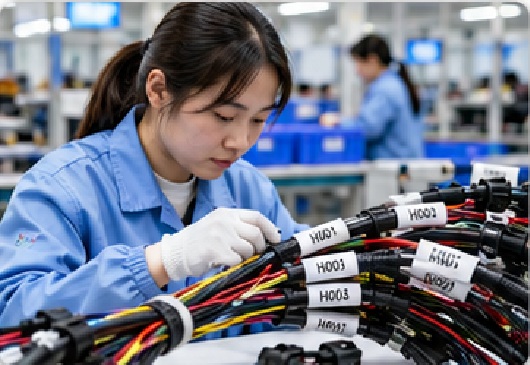
Wire Harness Assembly

Wire Harness Assembly

Harness programs can involve dozens or hundreds of identifiers across one assembly. Philiton can manage fixed and variable artwork, multiple cable diameters, color groups and pack sequences while keeping each SKU controlled. Labels can be prepared by harness family, work order or installation step to reduce sorting during assembly. Pilot quantities can also be grouped by cable family before the final label set is released for larger production.
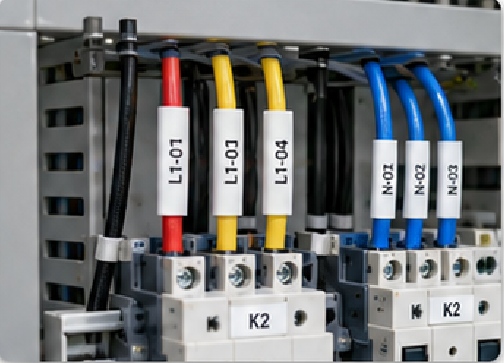
Electrical Panels

Electrical Panels

Control panels often need compact IDs that remain legible around terminals, cabinet wiring and service zones. Philiton reviews wire diameter, text size, color coding and installation method before choosing a wrap or self-laminating construction. Roll direction and dispensing format can also be matched to the workstation. When several cabinet versions share one label size, artwork and packing can still be separated by machine model or production order.
Telecom Cabling

Telecom Cabling

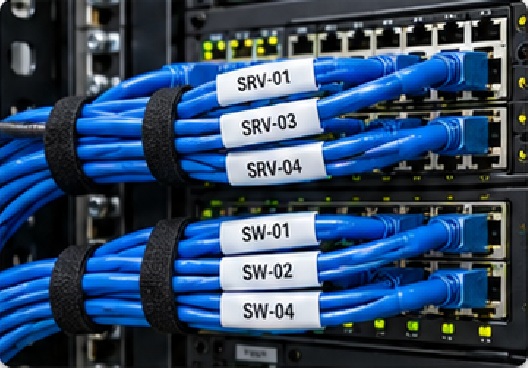
Telecom cable identification may combine route names, cabinet references, pair information, barcodes or QR codes. Philiton can organize multi-SKU production and variable data while keeping dimensions suitable for the cable OD and available viewing space. Sample application helps confirm the field remains readable after installation. Roll or sheet packs can be grouped by route, cabinet or work order when technicians need labels in a controlled installation sequence.
Data Centers

Data Centers

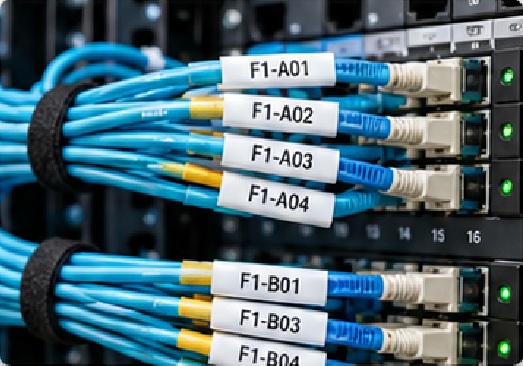
Data-center projects often require large identifier sets delivered in installation order. Philiton can structure data, artwork versions and packing by rack, row, cabinet or work package. Compact flag or wrap labels can be developed around cable density, scan requirements and field readability to reduce rework during deployment. A pilot pack can mirror one rack or cabinet so the final data layout is checked under real installation conditions before the full quantity is printed.
Automotive and EV

Automotive and EV

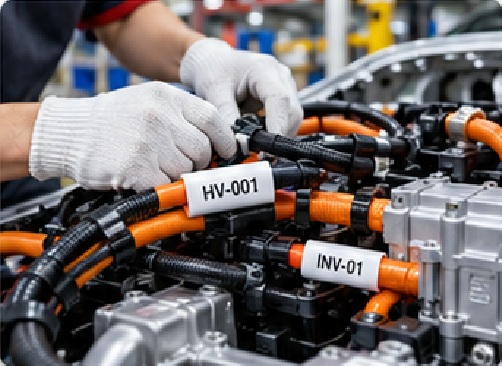
Automotive and EV cable identification can involve heat, oils, chemicals, vibration and traceability requirements. Philiton can support custom label manufacturing and variable data, while material performance and any regulatory requirement are confirmed for the exact cable, location and test condition before a specification is approved. Traceability fields, production lots and packaging rules can also be linked to the approved project specification when multiple vehicle or component variants are involved.
Industrial Equipment

Industrial Equipment

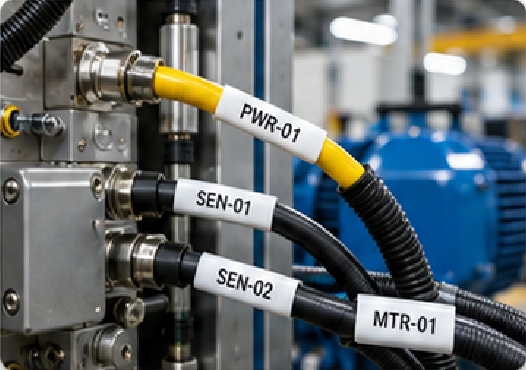
Machinery and industrial equipment projects may combine power, signal, sensor and communication cables in one system. Philiton can standardize label formats across cable groups while retaining separate artwork and data controls. Material, adhesive, abrasion protection and roll configuration are selected according to installation and maintenance conditions. When labels are replenished over time, retained specifications help keep repeat orders aligned with previous machine builds while still allowing controlled version changes.

Match Material and Adhesive to the Cable Jacket

A strong print result is not enough if the film is too stiff or the adhesive is poorly matched to the jacket, curvature, contamination and service environment.

Select the Construction From Surface, Flex and Exposure

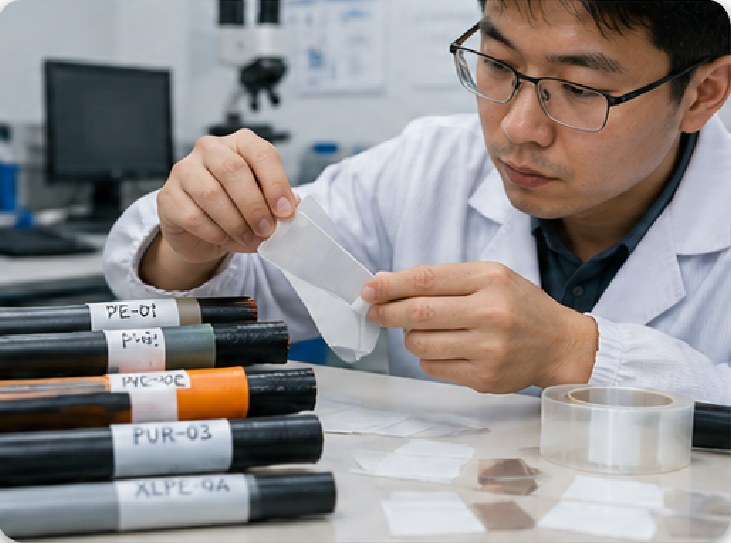
Philiton sources labelstocks according to project requirements and handles printing, converting, finishing, inspection and testing through its production system. Common candidate face materials can include PET, PP/BOPP, PE and other specialty films; higher-temperature electronics programs may also require project-specific specialty materials such as polyimide. The final choice depends on the cable jacket, required conformability, print method, overlamination or self-laminating structure, and expected handling.

Adhesive selection begins with the actual surface. Cable jackets can differ greatly in surface energy, texture, plasticizer content, flexibility and contamination. PE or other lower-surface-energy surfaces may need a different adhesive approach from a smoother, higher-energy surface. Curvature adds another load because the label is constantly trying to return to a flat shape, especially on smaller diameters.

Philiton therefore asks for cable material, OD, application temperature, service temperature, water or oil exposure, cleaning chemicals, outdoor use and required lifetime before locking the construction. When cable chemistry is unclear, a physical sample is more useful than a material name alone. Candidate labels can be applied, allowed to dwell and then checked for edge lift, movement, print protection and removal behavior. Material certificates or third-party test documents are reviewed against the exact selected construction rather than assumed from a general material family.

Define Durability by the Exposure, Not the Adjective

Terms such as waterproof, chemical-resistant or high-temperature only become useful when the actual exposure, duration, cable surface, service life and acceptance method are defined before material approval.

Service conditionWhat Philiton reviewsConstruction directionWhat should be validatedRelease decision
Repeated handling and abrasionContact points, rubbing, maintenance frequencyProtected print, laminate or self-laminating structureLegibility and edge condition after representative handlingApprove only after print remains readable
Water or condensationApplication temperature, moisture, dwell timeFilm stock plus suitable adhesiveAdhesion before and after moisture exposureConfirm on actual cable or equivalent surface
Oil or cleaner exposureChemical type, concentration, contact durationResistant film/ink/protective finish candidatePrint rub, swelling, edge lift and adhesive changeTest with representative chemical exposure
Outdoor installationUV, rain, temperature cycle, expected service periodOutdoor-suited film and adhesive candidateWeathering evidence or project test planDo not state outdoor life without supporting evidence
Elevated temperatureApplication and service temperatureHeat-capable material/adhesive candidateDimensional stability, adhesion and print durabilityConfirm against material data and sample test
Tight cable curvatureCable OD, film stiffness, overlapConformable film and suitable adhesiveSpring-back and edge lift after dwellApprove size/material combination, not material alone

Choose Pre-Printed or Locally Printable Labels

Both supply models are useful. The better route depends on how often data changes, where labels are applied, how many SKUs exist and who controls final print quality.

Factory Pre-Printed Labels

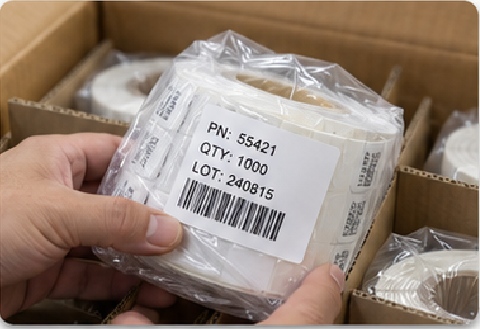
Factory pre-printed labels are suitable when identification data is known before production and consistent output is important across multiple sites or production batches. Philiton can print fixed text, sequential numbers, barcodes, QR codes and other variable fields, then die cut, inspect, rewind and pack labels by SKU or installation sequence. Centralized printing reduces the need for local printers, ribbons and template management. It also allows data verification and artwork control to be incorporated into the manufacturing workflow. Projects should define the source data, accepted file format, duplicate rules, reprint logic and packing sequence before variable production starts.
  • Best for fixed or controlled data sets
  • Suitable for multi-SKU and sequential production
  • Can be supplied in roll, sheet or individual formats
  • Data and artwork can be locked to an approved version

Customer-Printable Constructions

Locally printable labels are useful when identifiers are generated at the point of assembly, maintenance or field installation. Philiton can evaluate blank or partially pre-printed label constructions based on required printer technology, ribbon or ink system, label size, sensing method, liner, roll direction and print area. Printer compatibility must be confirmed from actual equipment specifications rather than assumed from a generic thermal-transfer label description. For programs mixing factory graphics with local variable data, the pre-printed area and printable field should be separated clearly so local printing does not interfere with coating, laminate, adhesive zones or sensor marks.
  • Best for changing job-site or production-floor data
  • Requires printer, ribbon and template compatibility review
  • Print area and sensor requirements must be defined
  • Pilot rolls are recommended before repeat supply

Control Variable Data Before It Reaches the Press

Cable identification often carries unique data. Philiton treats the data file, artwork template, production sequence and final verification as one controlled manufacturing workflow.

Sequential Wire IDs

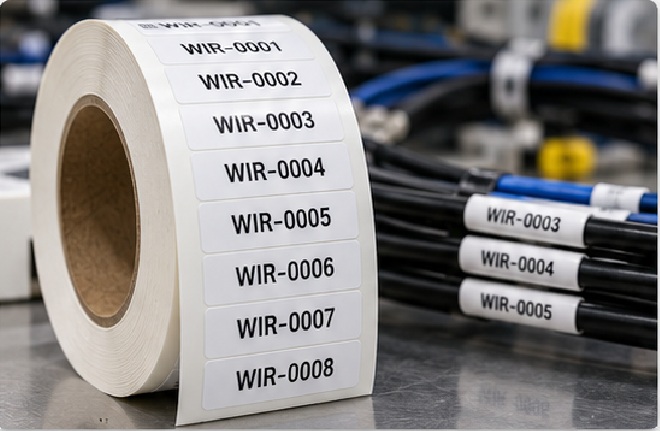
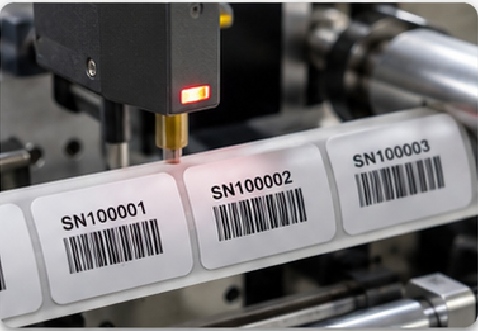
Sequential numbers should arrive with clear start/end rules, padding, prefixes, skipped values and repeat logic. Philiton can import or generate sequences according to the approved data rule, then check batch boundaries and reprints so an interrupted run does not quietly create duplicated IDs. For large harness programs, the sequence can also be segmented by SKU, work order or assembly family so production and packing stay traceable after printing.

Barcode Production

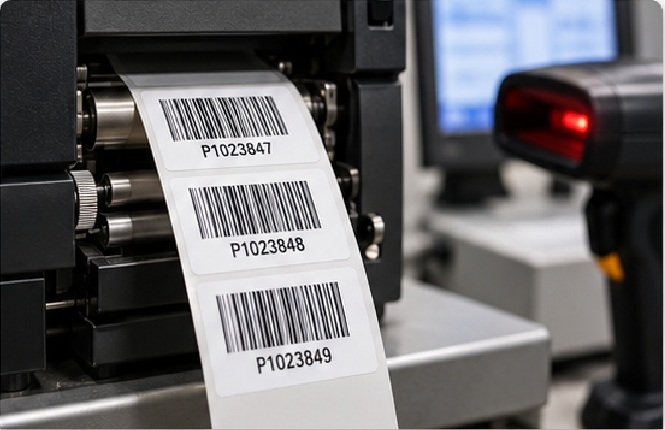
Barcode projects require more than visual sharpness. Symbology, size, quiet zone, human-readable text and expected scanner environment should be specified before artwork approval. Philiton can print variable barcodes and include scan or verification requirements in the QC plan when the project defines the acceptance method. When barcodes sit on a curved cable surface, code orientation and final wrap position are reviewed so the bars are not bent across an unsuitable radius.
QR Code Labels

QR Code Labels

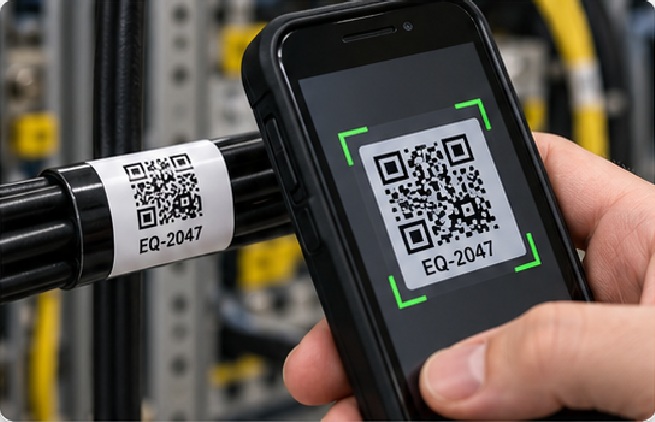
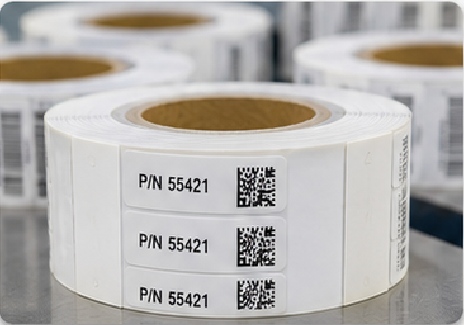
QR codes can carry asset links, installation references or other project data, but small cable labels leave little room for error. Philiton reviews code size, contrast, quiet zone and final curvature so the code is not compressed, folded, overwrapped or placed where the cable radius reduces reliable scanning. A printed pilot can be scanned after final application to confirm the code still works in the same geometry technicians will see in service.
SKU and Route Mapping

SKU and Route Mapping

Large installation programs may need identifiers grouped by harness, rack, cabinet, machine or work order. Philiton can organize production and packing around the same mapping used by the installation team, reducing sorting after delivery. Every artwork or data set remains controlled as a distinct production item even when materials are shared. Carton labels, roll labels and packing lists can follow the same route structure so receiving teams can reconcile the shipment without reopening every roll.

Send the Right Inputs for Faster Artwork Approval

Clear project inputs shorten quotation and sampling cycles, especially when small cable dimensions, variable data and roll configuration must work together.

Cable Outside Diameter

Provide OD in millimeters or inches for every cable family. For bundles, provide the finished bundle diameter rather than the diameter of one conductor. Photos beside a ruler help when the jacket is irregular, braided or highly textured. If several cable sizes share one proposed label, list the minimum and maximum OD so Philiton can check whether one wrap geometry remains workable across the range.

Cable Jacket Material

Identify PVC, PE, rubber-like, braided, painted or other known jacket material when possible. If the exact polymer is unknown, send a physical cable sample. Adhesive behavior can change with surface energy, texture, plasticizer and contamination. Also note any cleaning process, release agent, oil or handling residue that may be present when the label is applied, because a clean laboratory surface may behave differently from the production line.

Printed Information

Send fixed text, font constraints, symbols, barcodes, QR codes, serial numbers and any required color coding. Variable data is best supplied in a structured spreadsheet with one row per identifier and a stable field naming system. When several label sizes use the same database, mark which records belong to each format so artwork generation and production batches can be separated without manual interpretation.

Application Environment

List temperature during labeling, service temperature, indoor/outdoor use, water, oil, cleaning agents, abrasion and expected service period. Performance claims are only meaningful when the exposure condition is defined. If a chemical is involved, provide the product name or chemistry, concentration, contact frequency and approximate dwell time so candidate materials can be screened against a realistic condition instead of a generic chemical-resistance request.

Delivery Format

Confirm roll, sheet or individual pieces. For rolls, provide core size, inside/outside wound, unwind direction, maximum roll diameter, liner width, labels per roll, gap/pitch and any sensor mark or perforation requirement. If labels run through a desktop printer, industrial printer or dispenser, include the equipment model or its media specification so the finished roll can be reviewed against the actual feed path.

Quantity and SKU Plan

Provide quantity per artwork or data set, not only total order quantity. Similar SKUs can sometimes share materials and production setup, but each version still needs controlled artwork, quantity and packing identification. For launch programs, separate pilot quantity from expected repeat quantity so Philiton can choose an efficient sampling and production route without assuming the first run represents the long-term volume.

Sample the Risks That Could Stop Production Later

A cable-label sample should close fit, adhesion, print, data and dispensing risks before volume production rather than serve only as a color proof or artwork check.

Use Sampling to Lock the Manufacturing Specification
  • Philiton can separate sample goals according to project risk. A printed appearance sample confirms layout, text, color and die line. A material/application sample checks whether the construction wraps the cable, conforms to curvature and bonds to the jacket. A variable-data pilot verifies sequence, barcode or QR layout, and a roll-format sample checks core, winding, pitch, liner and dispensing behavior.

For standard printed label samples using confirmed artwork and readily available materials, scheduling commonly starts around 3-5 business days. Specialty adhesives, custom materials, complex converting or data-heavy pilots are quoted with a project-specific schedule. Sample timing begins after the information needed for the selected validation stage is complete; waiting for artwork, cable samples or specification approval is not active production time.

Before approval, Philiton recommends applying labels to representative cable, allowing adhesive dwell, then checking edge lift, readability, protective overlap, code scanning and handling. When the project runs through a local printer or applicator, the pilot should also be tested on the actual equipment. Once the approved structure is locked, material, artwork, tooling, data rules, roll parameters and QC criteria become the reference for mass production and repeat orders.

From Approved Artwork to Controlled Cable Label Production

Philiton links prepress, printing, converting, variable data, inspection and packing so every manufacturing step works from the same approved cable-label specification and revision.

Production Is Released Only After Critical Inputs Are Locked

Production begins with an artwork and specification review. The team checks label dimensions, print area, cable application, material, adhesive, colors, variable fields, die line, roll configuration and packing instructions. Digital printing can support short runs and multi-SKU work, while flexographic and other printing routes can be selected when quantity, material and repeat-production economics justify a different setup. Screen, UV and other specialty processes are available for projects that require specific graphics or durable print effects.

After printing, converting controls determine whether the approved design becomes a usable cable-identification product. Lamination or a self-laminating clear zone may protect print; die cutting defines wrap geometry; waste stripping removes matrix; slitting and rewinding set liner width, core, winding direction and finished roll size. Variable-data programs add data import, batch control, stoppage/restart rules, reprint handling and final sequence checks.

Mass production is not treated as a larger copy of a sample. Philiton compares production against the approved artwork/specification and project QC plan, then packs by SKU, quantity and batch. Repeat orders can reuse retained project records when the specification remains unchanged, while changed cable size, jacket, material, data structure or compliance requirement triggers a fresh review before release.
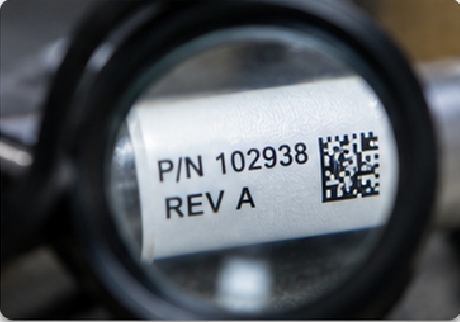
Quality Checks Focused on Cable Identification Performance

Philiton combines routine print and converting control with cable-specific checks so readable artwork also arrives in a format that can be applied, scanned and traced.
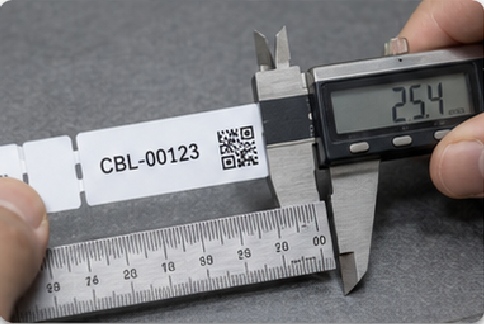
Dimension and Die Cut

Dimension and Die Cut

Finished width, length, printable zone, clear overlap and die-cut position are checked against the approved specification. Small shifts matter on narrow wire labels because an overlap can move onto text or reduce the adhesive area available around the cable. Where a fold or flag geometry is used, fold position and symmetry are also checked so the readable field lands where the approved sample showed it.

Print Legibility

Text, symbols and small characters are reviewed for readability at the approved size. Fine industrial IDs are not judged only from a computer file; print gain, material surface and final viewing distance can change the result. Where a code or symbol sits close to an edge, die-cut tolerance and protective overwrap are considered together so critical information is not clipped or covered after application.

Variable Data Control

Sequential numbers, barcodes, QR codes and other changing fields are controlled through source data, production batches, stoppage/restart handling, reprints and final checks. The goal is to prevent missing, duplicated or mixed identifiers from reaching assembly. For segmented projects, accepted quantities can also be reconciled by SKU or data range before packing so each roll corresponds to the intended installation group.

Adhesion and Wrap Fit

Project-level application checks can be performed on supplied cable or representative surfaces. The review focuses on conformability, spring-back, lifting edges, overlap position and whether the label remains stable after the agreed dwell period. If the cable is handled, flexed or exposed to cleaners in service, the sample plan can include representative handling or exposure before the structure is approved for production.

Roll Configuration

Core, winding direction, inside/outside wound, liner width, gap/pitch, roll diameter and labels per roll are checked when those parameters affect a printer, dispenser or workstation. A correct label on the wrong roll can still stop an assembly process. Finished rolls can be compared with the approved unwind diagram and equipment limits before cartons are closed, reducing avoidable line-side setup problems.

Final Packing Check

Finished rolls, sheets or individual pieces are identified by SKU, quantity and batch as required. Mixed-SKU projects are kept traceable through packing so receiving teams can reconcile cartons with the order and installation plan. Packing instructions can also define roll sequence, carton sequence, pallet grouping or zone-specific labels when installation teams need materials released in a particular order.

Specify Roll and Packing Details Before Production Starts

Roll configuration affects printers, dispensers, storage and line-side handling. Philiton records delivery parameters together with the label specification instead of deciding them after printing.

Delivery parameterWhat to provideWhy it mattersPhiliton control point
Core diameterRequired core ID from printer/applicatorControls machine fit and roll buildConfirm before rewinding
Winding directionInside/outside wound and leading edge orientationControls how label enters printer or dispenserMatch approved unwind diagram
Gap and pitchSensor spacing or indexing requirementAffects detection and registrationCheck die-cut repeat against specification
Maximum roll ODMachine or storage limitControls labels per roll and total roll thicknessSet roll count during rewinding
Liner widthRequired web width and side marginsAffects tracking through printer/applicatorControl slitting width
Labels per rollTarget count or roll lengthSupports workstation replenishment and inventoryCount and label each roll
SKU separationOne SKU per roll/carton or mixed rulesPrevents installation and receiving errorsUse SKU/batch carton identification
Shipment methodCourier, air or sea plus destinationDetermines packing protection and logistics quoteQuote route and transit separately by project

Flexible Quantities Without Losing the Scale-Up Path

Philiton can support many standard custom label projects from around 500 pcs, while final MOQ follows material, process, SKU count, tooling and supply-chain requirements.

Trial and Qualification Runs

Small initial runs are useful when cable material, label geometry or data layout still needs validation. Digital production can reduce setup pressure for many standard label constructions, but every SKU still needs approved artwork and quantity control. Special materials or dedicated tooling may require higher starting quantities. A trial order can also isolate one cable family or one installation zone before the same construction is expanded across the full program.

Multi-SKU Production

Cable projects often contain many identifiers with the same material and shape. Compatible SKUs can sometimes share stock and production setup, while each artwork or data set remains separately controlled. Quantity should therefore be planned per SKU, not only as one total order number. Grouping similar SKUs can improve material use and production efficiency without merging the artwork, quantity or QC identity of each finished item.

Repeat Production

Once artwork, material, adhesive, die line, roll format and QC criteria are approved, repeat orders can move through a faster review because the production reference already exists. Any change in cable, data, environment or compliance requirement is checked before the previous specification is reused. Retained records also help purchasing teams compare a new order with the previous version instead of rebuilding technical details from email history.

Volume Scaling

The same manufacturing chain can move from short-run digital production into larger repeat programs using the printing and converting route that best fits quantity and specification. Philiton’s manufacturing system is designed to support controlled scale-up rather than forcing a supplier change after qualification. Larger quantities can also be reviewed for roll count, packaging, batch planning and delivery method so scale improves unit economics without changing the approved application performance.

Documentation Must Match the Exact Label Construction

Cable and wire programs often mention UL, RoHS, REACH, flame behavior, chemical resistance or temperature ratings. Philiton separates manufacturing capability from documentary claims so evidence stays tied to the actual material and use condition.

Build the Compliance File Around the Finished Specification

Philiton can manufacture to approved regulatory artwork and can support material documentation or third-party testing when the project requires it. Evidence must be connected to the selected face material, adhesive, ink, protective layer, cable application and destination requirement. A report for one film or adhesive should not automatically be extended to another construction after a material, supplier or end-use change.

ISO, FSC, UL, IATF, BSCI, Sedex/SMETA, GRS and similar certifications are not presented as active Philiton certifications unless the certificate number, scope, legal entity and validity are verified for publication. RoHS and REACH are also not treated as generic factory certificates; they relate to defined materials, substances, test scope and market requirements.

For projects that need a formal document package, send the target standard, destination market, cable application and any project specification during the quotation stage. Philiton can then determine which supplier documents, material declarations, test reports, production records or third-party testing should be included. The brand, importer or legally responsible product party remains responsible for confirming final market-entry and labeling obligations.
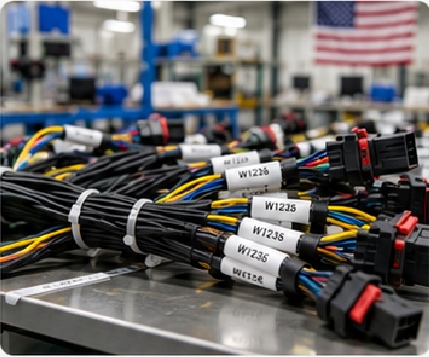
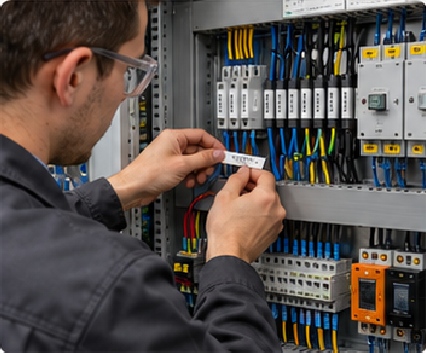
Representative Cable Label Project Configurations

The following anonymized examples show how Philiton can structure cable-identification orders. They illustrate manufacturing logic without naming brands or claiming unverified public case histories.
United States Wire Harness Program

United States Wire Harness Program

An industrial wire-harness brand in the United States can require 12,000 self-laminating labels across multiple cable IDs for equipment assemblies. A workable project starts by grouping cable diameters, locking one printable field for each size family, and mapping sequential data to the harness bill of materials. Philiton can run a printed pilot, apply labels to representative cable, check clear-overlap coverage and scan performance, then release production by SKU. Finished rolls can be separated by harness family and carton-marked by work order so assembly teams receive identifiers in a controlled sequence rather than one mixed bulk carton.
Germany Automation Equipment Program

Germany Automation Equipment Program

A German automation-equipment manufacturer can source 8,500 wrap-around wire labels for control cabinets and machine wiring. The project may combine fixed equipment codes with changing terminal or circuit identifiers, requiring artwork templates plus structured variable data. Philiton can review wire OD, jacket surface, character size, roll direction, core and pitch before sampling. After the approved sample locks material, adhesive, die line and print position, mass production can be split by machine series and packed with clear SKU identification. Repeat orders can then reference the retained specification while new cabinet versions receive separate artwork and data approval.
Australia Data Center Program

Australia Data Center Program

An Australian data-center integrator can order 18,000 cable flag and compact wrap labels for rack, cabinet and patch-cable identification. The project may include rack IDs, port references, QR codes and installation-zone mapping. Philiton can organize the source spreadsheet by row, rack and cabinet, then produce a pilot set to verify code size, fold position and readability on the selected cable. Production can be packed by deployment zone instead of only by label type, helping site teams reduce sorting. Any revised rack plan is treated as a new controlled data version before additional labels are released.

Manufacturing Depth for Repeat Industrial Label Programs

Philiton combines flexible order quantities with a manufacturing system built for artwork control, printing, converting, inspection and repeat production across industrial identification projects.

Established Manufacturing Base

Philiton was founded in 2016 and operates manufacturing facilities in Shenzhen and Dongguan, China. The combined manufacturing system covers more than 12,000 ㎡ and supports custom labels, stickers, tags, industrial identification, security labels and smart-label projects for international programs. Cable and wire identification sits within the company’s broader electronics and industrial-label scope, allowing related barcode, QR, variable-data and durable-label requirements to be handled within the same manufacturing organization.

200+ Person Organization

More than 200 employees support the manufacturing operation. Among them, 91 are technical personnel, experienced machine operators and quality-related staff responsible for process execution, print consistency, finishing, testing and inspection across different production stages. The staffing structure supports projects that need coordination between artwork, printing, converting, data control, QC and packing rather than treating each step as an isolated subcontracted task.

Multi-Process Production

Philiton’s production capabilities cover artwork and prepress, digital printing, flexographic and other label printing, screen and UV processes, variable data, lamination, die cutting, slitting, rewinding, automated inspection, laboratory testing, packing and shipment preparation. Materials are sourced externally to match project needs. The manufacturing value therefore sits in selecting, converting, printing, validating and controlling the chosen construction rather than claiming that base films, adhesives or specialty substrates are produced in-house.

Short Runs to Repeat Scale

Many standard custom label and sticker projects can start from around 500 pcs, subject to material and process. The same manufacturing chain can support sample development, multi-SKU launches and repeat mass-production programs, allowing an approved cable-label specification to scale without changing manufacturing partners. For larger programs, production planning can incorporate batch size, roll configuration, SKU separation and shipment scheduling so commercial scale increases without losing the controls established during qualification.

Cable & Wire Labels Frequently Asked Questions

Start with cable outside diameter, jacket material if known, application environment, printed information, quantity per SKU and preferred delivery format. If the cable surface is unusual or the diameter is small, a physical cable sample can make material and sizing decisions more reliable.
Yes. Philiton’s product scope includes self-laminating cable labels, wire wrap labels, wrap-around cable labels, cable flag labels and cable tags. Final structure, material, adhesive and dimensions are confirmed from the actual cable and application requirements.
Sizing starts with cable OD and circumference, then adds the required printable field, overlap and any protective clear section. Final dimensions are checked against the actual cable because material stiffness and jacket surface affect wrap behavior.
Yes. Philiton supports variable data such as sequential IDs, barcodes and QR codes. The data source, field rules, duplicate handling, reprint logic and verification method should be defined before production starts.
Blank or partially pre-printed constructions can be evaluated when printer technology, ribbon or ink, sensing method, core, winding direction, label pitch and printable area are known. Pilot rolls are recommended before repeat supply.
Many standard custom label projects can start from around 500 pcs, but cable-label MOQ depends on material, adhesive, label size, number of SKUs, printing process, tooling and whether special stock must be sourced.
Standard printed samples using confirmed artwork and available materials commonly begin around 3-5 business days. Specialty materials, adhesives, complex converting or variable-data pilots receive a project-specific schedule after the specification is reviewed.
Candidate constructions can be selected for oil or chemical environments, but the chemical type, concentration, contact duration, temperature and acceptance criteria must be defined. Final resistance claims should be supported by material data or project testing.
Labels can be packed as rolls, sheets or individual pieces. Rolls are protected against crushing, moisture, telescoping and unwinding, and cartons can identify SKU, quantity and batch. Courier, air and sea shipment can be arranged according to destination and urgency.
Yes, when approved artwork, material, adhesive, tooling and production parameters are retained and unchanged. Every reorder is still reviewed for quantity, cable, data, compliance or packing changes before release.

Send Your Cable Label Specification for Review

A useful quotation starts with the cable and application, not only the finished label dimensions. Send available information and Philiton can organize the remaining items before sampling. For cable-identification projects, the most useful inputs are cable outside diameter, jacket material or a physical sample, label type, printed content, variable-data file, quantity per SKU, operating environment, application method and required roll or sheet format. For printer- or dispenser-fed labels, include core size, winding direction, maximum roll diameter, liner width, gap/pitch and any sensor requirement. If oil, chemicals, outdoor exposure, elevated temperature or compliance documentation is involved, include the exact condition and target standard so material selection and testing can be planned correctly. Also include the destination country, preferred shipping method and required in-hand date when timing matters. Philiton can then separate sample preparation, active production and logistics timing instead of giving one combined lead-time estimate that hides where approval or transport time is being spent.

  • Cable OD and jacket material
  • Label type or application photo
  • Artwork, text, barcode or QR requirements
  • Variable-data spreadsheet, if applicable
  • Quantity per SKU or data set
  • Temperature, water, oil, chemical and abrasion conditions
  • Roll, sheet or individual-piece delivery format

For all inquiries, please feel free to reach out at:

Get In Touch

  • Our team will answer your inquiries within 12 hours.

  • Your information will be kept strictly confidential.

Get a Fast Quote for Custom Labels & Stickers

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”. 
For all inquiries, please feel free to reach out at:

Ask For A Quick Quote

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”. 
For all inquiries, please feel free to reach out at:

Get a Quote Today!

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”.