Your Trusted Labels & Stickers Manufacturer from China!

Label Factory Manufacturing for Custom Labels and Stickers

Built for brands, manufacturers and channel partners that need controlled label production from artwork review through repeat manufacturing.

Philiton combines flexible project entry with a broad manufacturing chain for labels, stickers, tags and specialty printed products.
  • 12,000+ ㎡ manufacturing footprint across Shenzhen and Dongguan
  • 200+ employees, including 91 technical, skilled production and quality personnel combined
  • Many standard custom label and sticker projects can start from approximately 500 pcs
  • Digital, flexographic, screen, UV, variable data, specialty finishing, converting, inspection and testing capabilities
Label Factory Manufacturing for Custom Labels and Stickers

Factory Facts That Matter Before Supplier Qualification

A manufacturing partner should be assessed by what can be verified: production scope, people, process depth, quality controls and the ability to support projects as volumes change.

Shenzhen And Dongguan Manufacturing

Philiton operates manufacturing facilities in Shenzhen and Dongguan, China. The dual-location manufacturing structure supports multiple production functions, project coordination and different label programs without presenting the business as a simple online sticker reseller. Specific factory addresses are shared at the appropriate project stage when an audit, factory visit, sample confirmation or commercial review requires them. The public manufacturing message stays focused on verified operating locations and production responsibility rather than unsupported claims about site-by-site capacity.

12,000+ ㎡ Manufacturing Footprint

The combined manufacturing footprint is approximately 12,000+ ㎡. The space supports label production activities across artwork and prepress, printing, finishing, converting, inspection, testing, packing and shipment preparation. Floor area is useful only when connected to actual production work, so Philiton does not convert the number into unverified monthly output claims. For a sourcing team, the more relevant question is whether the factory has enough process depth to move a project from material selection and proofing into controlled repeat production.

200+ Employees

Philiton employs more than 200 people across the manufacturing organization. Functions cover sales coordination, artwork and prepress, technical review, machine operation, converting, quality, warehousing, packing, maintenance and management. Headcount is not presented as a guarantee of unlimited capacity. Its value is the ability to coordinate multiple production steps internally and keep technical, production and quality responsibilities connected when a label moves from approval into bulk manufacture and later repeat orders.

91 Core Production Professionals

Technical personnel, skilled machine operators and quality-related staff total 91 people. Philiton uses the combined number rather than inventing separate engineer, press-operator or QC counts that have not been formally verified. For complex projects, this group supports process execution, equipment operation, print consistency, finishing quality, inspection and testing. The structure is especially relevant when a program involves multiple SKUs, variable data, roll configuration, difficult materials, decorative finishing or application requirements that need coordination across more than one production step.

Flexible Project Entry

Many standard custom label and sticker projects can start from approximately 500 pieces, subject to material, printing method, finishing, size, SKU structure and tooling. The figure is not a universal MOQ for RFID, dedicated holograms, special adhesives, unusual face stocks or complex security constructions. The commercial advantage is a controlled entry point for launch runs, regional versions, new SKU validation or supplier trials while preserving access to the same broader manufacturing system when reorder quantities become larger.

Integrated Manufacturing Scope

Philiton’s production system covers artwork and prepress support, digital and conventional printing, flexographic printing, screen and UV processes, variable data, foil, embossing and debossing, holographic effects, lamination, die cutting, slitting and rewinding, automatic inspection, laboratory testing, packing and shipment preparation. Base raw materials are sourced from external suppliers. Philiton’s manufacturing value lies in selecting, converting, printing, finishing, inspecting and managing those materials according to the approved project specification.

Manufacturing Support For Different Procurement Programs

Different organizations evaluate a label factory for different reasons. Philiton structures project support around launch risk, production fit, repeatability, technical requirements and commercial scale.

Growing Multi-SKU Brands

Brands launching several products at once often need lower inventory exposure without losing access to professional production controls. Philiton can review shared materials, compatible finishing, common roll specifications and artwork differences across SKUs, while each design remains independently approved and identified for QC. A typical discussion covers launch quantity, expected reorders, surface and container differences, color targets, version control and whether later volume could justify a different print route. The goal is not simply a low starting quantity; it is a manufacturing path that avoids rebuilding the supply chain after growth.

Established Consumer Brands

Established brands usually place more weight on repeatability, appearance, packaging-line compatibility and change control. Philiton can organize artwork review, material selection, approved samples, color and finishing references, roll configuration, final inspection and repeat-order checks around a locked specification. When packaging artwork changes, the project can be re-reviewed rather than automatically copying a previous job. This approach suits cosmetics, food and beverage, home fragrance, supplements, personal care and other categories where packaging presentation and SKU management directly affect launch timing and retail execution.

Manufacturers And OEMs

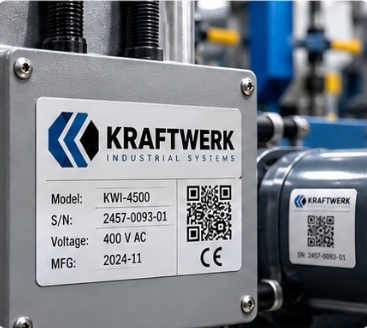
Manufacturing companies often need labels to function inside a production system, not simply look attractive. Key inputs can include application surface, surface energy, temperature, oil or chemical exposure, barcode or QR requirements, roll direction, core size, gap, maximum roll diameter and applicator conditions. Philiton can connect those inputs to material, adhesive, printing, converting and inspection choices. For industrial, electronics, automotive, cable, battery or equipment programs, production reliability and traceability usually carry more weight than decorative effects alone.

Packaging Companies And Brokers

Packaging companies, distributors and print brokers need a manufacturing backend that can support multiple end projects without exposing confidential relationships. Philiton can work with white-label arrangements, neutral packaging, blind-shipping requirements, NDA-controlled artwork and project-specific commercial terms where agreed. Technical information can be organized so the channel partner receives material, print, finishing, roll and quality information needed to serve the end account. Each project still requires clear ownership of artwork approval, specifications, delivery instructions and end-use requirements.

Enterprise Procurement Programs

Larger organizations evaluate more than price. Supplier qualification can involve factory identity, incoming material control, artwork revision, process checks, inspection, traceability, document scope, confidentiality, audit support and change management. Philiton can structure project records around approved artwork, specifications, samples, inspection outputs, packing information and shipment records. Certification, performance and compliance claims are handled by actual document scope rather than blanket statements. This gives procurement, packaging, engineering and quality teams a clearer basis for deciding which parts of a program are ready for approval and which still require project-level verification.

What To Check When Qualifying A Label Factory

Qualification AreaWhat To VerifyPhiliton Manufacturing BasisProject-Level Confirmation
Manufacturer IdentityReal production responsibility, not only sales or outsourcingManufacturing operations in Shenzhen and DongguanFactory visit or audit scope when required
Manufacturing ChainPrinting, finishing, converting, inspection and packing depthArtwork/prepress through printing, converting, QC and shipment preparationExact process route for the selected label
Material ControlFace stock, adhesive, liner and special material sourcingExternal qualified material sourcing plus incoming and production controlMaterial brand, certification or special performance when needed
Artwork ControlDieline, version, white ink, foil, variable data and barcode handlingArtwork and prepress support before productionFinal approved file and revision
Print TechnologyAbility to match quantity, material and visual targetDigital, flexographic, screen, UV and other production routesSelected press route after specification review
FinishingDecorative and functional post-print capabilityFoil, emboss/deboss, holographic effects, lamination, die cutting and moreTooling, material and effect approval
Automatic ApplicationRoll direction, core, gap and roll diameter compatibilitySlitting, rewinding and roll configuration supportApplicator specification and line trial if needed
InspectionPrint, die cut, code and roll defect controlAutomatic vision inspection capability plus quality checksInspection level agreed for the project
TestingAdhesion, color, durability, barcode or application checksIn-house testing capability for relevant project verificationExact method, acceptance criteria and report scope
Security / Smart LabelsVariable data, tamper evidence, RFID or NFC manufacturing supportSecurity processing, encoding and functional verification capabilitiesChip, inlay, data, read range and security requirements
Scale-UpAbility to move from pilot to repeat productionFlexible entry quantities plus digital and volume manufacturing routesForecast, repeat volume and changeover strategy
ConfidentialityControl of artwork, brands, samples and project dataNDA and project-based access/control proceduresContract scope and data handling requirements

Labels And Stickers Manufactured Across Commercial Applications

Philiton supports packaging, identification, promotional, industrial, security and smart-label projects. Each category is engineered around application surface, environment, artwork, quantity and delivery format.
Pressure-Sensitive Labels

Pressure-Sensitive Labels

Pressure-sensitive labels cover a broad range of paper and film constructions for bottles, jars, cartons, pouches, equipment and retail packaging. A workable construction depends on more than the face material: adhesive, liner, print process, coating or laminate, die cut and application method all affect performance. Philiton reviews the container or substrate, labeling temperature, service environment and required appearance before the production structure is finalized. Labels can be supplied in rolls, sheets or individual formats according to the application process.
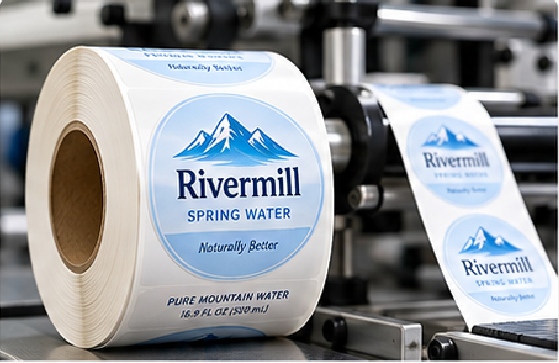
Roll labels are designed around both the printed label and the downstream labeling process

Roll Labels

Roll labels are designed around both the printed label and the downstream labeling process. Important inputs include web width, roll direction, core size, gap, maximum roll diameter, liner, rewind direction and whether the label will be hand applied or machine applied. Philiton can print, die cut, inspect, slit and rewind roll labels to an agreed configuration. Automatic applicator projects should include machine requirements early, because a visually correct label can still create production problems if the roll specification is wrong.
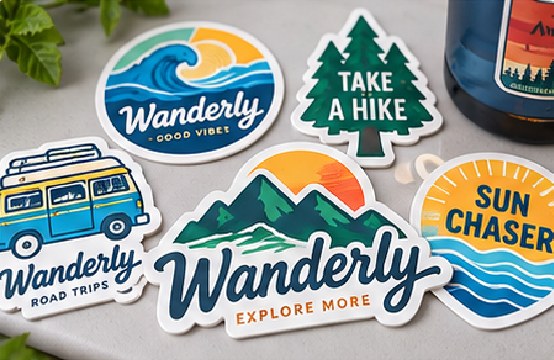
Die-cut stickers use a custom or standard contour to follow the artwork rather than a simple rectangular format. Vinyl, PP/BOPP, PET, paper and specialty materials can be selected depending on intended use.

Die-Cut Stickers

Die-cut stickers use a custom or standard contour to follow the artwork rather than a simple rectangular format. Vinyl, PP/BOPP, PET, paper and specialty materials can be selected depending on intended use. Production decisions include kiss cut versus through cut, liner margin, corner detail, small internal shapes, print bleed, laminate or varnish, and packing format. For brand programs, consistent contour and edge quality matter because the shape itself often becomes part of the visual identity.
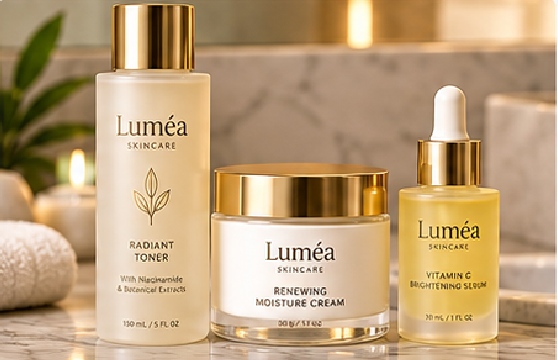
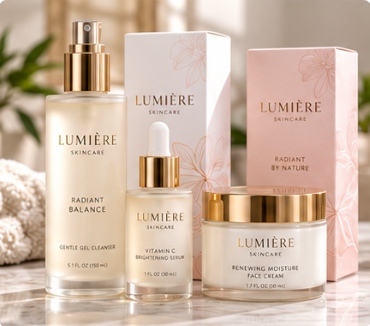
Cosmetic and skincare labels frequently combine strong visual requirements with moisture, oil, curved containers, transparent packaging or small-diameter surfaces.

Cosmetic Labels

Cosmetic and skincare labels frequently combine strong visual requirements with moisture, oil, curved containers, transparent packaging or small-diameter surfaces. Clear films, white films, metallic structures, textured papers, white ink, foil, embossing, spot effects and protective laminates can be evaluated according to the package. Multi-SKU programs also need disciplined artwork control so ingredient panels, shades, sizes or language versions do not become mixed. Sampling on the real bottle or a representative surface is useful when clarity, adhesion or wrap performance is critical.
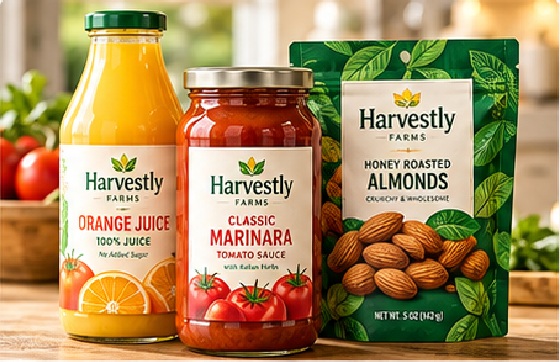
Food And Beverage Labels

Food And Beverage Labels

Food and beverage programs can involve bottles, cans, jars, tubs, pouches, chilled products, frozen products and dry packaging. Selection starts with package material and temperature conditions rather than assuming one waterproof structure fits every use. Paper may suit dry environments; film structures can be better for moisture, oil or condensation depending on the construction. Philiton can combine printed appearance, adhesive choice, protective finishing, roll format and barcode requirements while keeping any food-contact or regulatory claim tied to the actual material documentation and project scope.
Wine And Spirits Labels

Wine And Spirits Labels

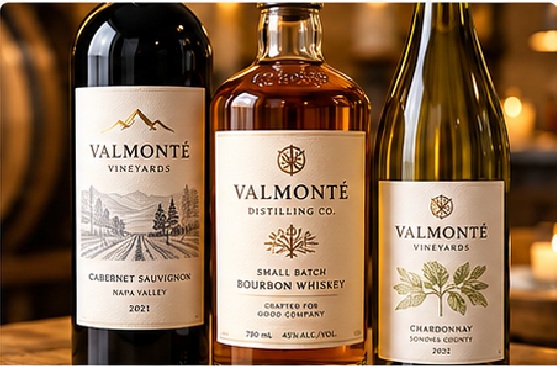
Wine and spirits labels often depend on tactile and decorative choices as much as print color. Textured papers, metallic films, foil stamping, embossing, debossing, spot UV and complex die cutting can create premium effects, but every added process changes tooling, registration, cost and production control. Bottle surface, condensation, ice-bucket exposure and application conditions should be reviewed before material approval. A production-intent sample is especially useful when several decorative processes must register precisely on the same design.
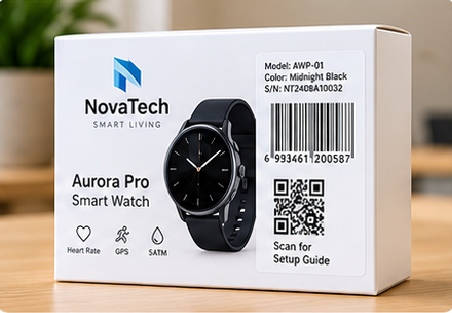
Thermal And Logistics Labels

Thermal And Logistics Labels

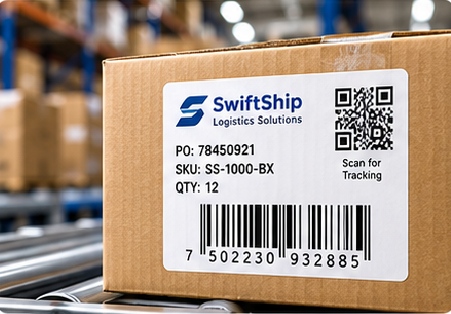
Thermal, shipping, warehouse and inventory labels are recurring operational products where scan quality, roll configuration and material compatibility often matter more than decorative finishing. Direct thermal and thermal-transfer structures can be selected according to print method, service life, abrasion, handling and exposure. Barcode size, quiet zones, contrast, variable data and liner/roll setup should be confirmed before production. Philiton can support recurring programs where SKU control, roll identification, packing and repeat-order consistency are important to warehouse or logistics operations.
Barcode And QR Labels

Barcode And QR Labels

Barcode and QR labels require both readable print and disciplined data handling. The artwork must preserve code dimensions, contrast, quiet zones and print clarity, while variable-data jobs also need sequence control and verification against the supplied data file. Material, varnish or laminate should not reduce scan performance. Philiton can combine variable printing, inspection and data matching according to the project. Acceptance criteria should be agreed before bulk production if a specific barcode grade, scanner environment or database-matching requirement applies.
Industrial Labels

Industrial Labels

Industrial labels are commonly used on machinery, tools, electronics, components, chemical products and factory assets. Selection can involve durable PET or other films, stronger adhesives, abrasion protection, serial numbers, warning information and machine-readable codes. The required construction depends on the actual surface, temperature, oil, chemicals, outdoor exposure and service life. Philiton can help translate those conditions into a material and print route, while exact resistance values remain tied to the chosen construction and agreed test conditions.
Automotive And EV Labels

Automotive And EV Labels

Automotive and EV applications can include component labels, battery labels, cable labels, warning labels, tracking labels and service identification. Projects may require resistance to heat, oil, chemicals, abrasion or long-term handling, but final performance must be validated against the exact material and environment. Philiton can support variable data, QR or barcode identification, durable face stocks, adhesive review, protective finishing and production inspection. For line-applied labels, roll configuration and traceability requirements should be defined alongside the printed design.
Security And Tamper Labels

Security And Tamper Labels

Security labels can use VOID transfer, destructible constructions, security seals, holographic elements, serial numbers, scratch-off structures or unique codes depending on the threat model. The correct solution depends on what the program is trying to reveal, prevent or trace. Philiton can combine printing, security materials, coding, converting and inspection, but security should not be reduced to a decorative hologram. Brand-protection projects work best when the authentication method, distribution risk, expected tampering behavior and verification process are defined before production.
RFID And NFC Labels

RFID And NFC Labels

RFID and NFC labels add an inlay, chip and data function to the printed label construction. Philiton supports printing, converting, encoding and functional verification for suitable RFID/NFC programs used in retail, apparel, assets, logistics, authentication and smart packaging. Chip family, frequency, inlay layout, read range, encoding rules and system integration are not assumed to be universal. Those details are confirmed by project so the physical label, data content and read environment are evaluated together rather than treated as a standard printed sticker.

How A Label Order Moves Through Manufacturing

A controlled label program moves through defined gates. Each stage closes a different risk before material, artwork or production is allowed to progress.

Requirement Review

The project starts with size, shape, quantity, SKU count, application surface, expected environment, artwork status, finishing, delivery format and destination. Automatic application adds roll direction, core, gap and roll diameter requirements. Security, RFID or variable-data work adds data and verification inputs. Missing information is not silently guessed when it can change material or tooling. The first output is a clearer manufacturing specification that can be used for material selection, quotation and sample planning.

Material Structure Selection

Face stock, adhesive, liner and protective structure are selected around the application rather than around a material name alone. Paper, BOPP/PP, PET, PE, thermal, metallic, clear, holographic or textured structures may be considered. Surface energy, curvature, moisture, oil, temperature and removability can change adhesive requirements. Special materials or certified constructions may need project sourcing and document verification. The output is a proposed material route that can move into proofing, sampling or application testing.

Artwork And Prepress

Approved design files are converted into production-ready information. Dielines, bleed, color separations, white ink, foil, embossing, variable-data areas, barcode dimensions and cutting paths are checked before release. If the design creates a manufacturability issue – for example very small reverse text, thin foil lines or a die-cut detail too close to the edge – the risk should be raised before tooling and production. The output is a controlled artwork version rather than a visual PDF with unclear production layers.

Sampling And Proofing

Sampling is used to close the highest-risk variables before bulk manufacture. A project may need a digital print proof, material sample, production-intent sample, finish sample or application test depending on the requirement. Sample timing is confirmed after material availability, tooling, finishing and smart-label components are reviewed; Philiton does not apply one fixed lead time to every specification. The output should be a clear approval reference covering the relevant dimensions, material, color, finishing and functional requirements.

Customer Approval

Approval freezes the production reference. Artwork revision, size, material, adhesive, print target, finishing, die cut and roll configuration should be confirmed before bulk release. For complex work, approval may include multiple dimensions rather than a single “looks good” message. A later change to artwork, material, supplier batch, finishing or application conditions can require re-evaluation. The goal is to avoid discovering a specification difference after materials have been prepared or production has already started.

Printing And Converting

Production follows the approved route using the selected printing and post-print processes. Depending on the job, work can include digital or flexographic printing, screen or UV processes, variable data, foil, embossing, lamination, die cutting, waste stripping, slitting and rewinding. Each added process creates its own control points for registration, material tension, surface appearance or tooling. The manufacturing route is chosen around the specification rather than forcing every job through the same technology.

Inspection And Packing

Quality checks are performed through the production route and again before packing. Inspection can cover print defects, contamination, registration, die cutting, waste removal, barcodes or QR codes, roll configuration and selected variable-data requirements. Vision inspection is available for applicable roll-label projects, while destructive or performance testing is handled according to agreed sampling and test scope. Finished labels are then identified, separated by SKU and packed in the correct roll, sheet or individual format.

Shipment And Reorder Control

After final QC and packing, shipment information is checked against quantity, carton count, destination, trade term and logistics route. Commercial invoices and packing lists can be prepared for export shipments. Repeat orders are reviewed rather than automatically released: artwork, material, adhesive, tooling, quantity and delivery conditions should be checked for changes. When the approved specification remains stable and materials are available, repeat manufacturing can usually be prepared more efficiently than a first-time development program. 
Material Families For Different Label Environments

Material selection starts with the package, environment and labeling process. Philiton sources label stocks externally and converts them into the approved finished construction.
Coated paper is widely used for dry packaging, retail products, cartons, jars and general product identification where a clean printed surface and controlled cost are important.

Coated Paper

Coated paper is widely used for dry packaging, retail products, cartons, jars and general product identification where a clean printed surface and controlled cost are important. It can support conventional color printing and many decorative finishes. Paper is not automatically the right choice for heavy moisture, oil or repeated abrasion. Adhesive, coating or laminate may improve performance, but the complete construction should be evaluated against the application rather than treating “paper label” as a single fixed specification.
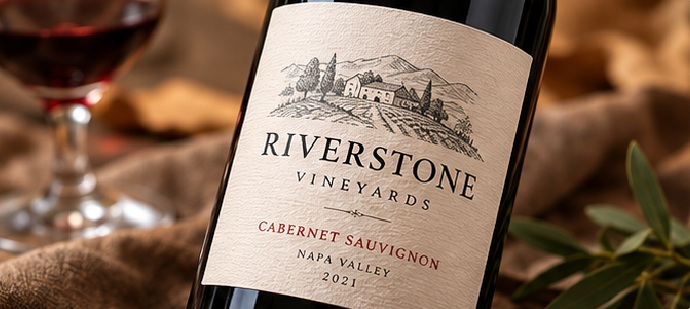
Uncoated and textured papers are selected when touch, natural appearance or premium presentation matters. They are common directions for wine, spirits, candles, specialty food, gifts and boutique packaging.

Uncoated And Textured Paper

Uncoated and textured papers are selected when touch, natural appearance or premium presentation matters. They are common directions for wine, spirits, candles, specialty food, gifts and boutique packaging. Surface texture can influence ink laydown, fine text, foil registration and barcode readability, so artwork and finishing should be reviewed with the material. Exposure to water, oil or condensation also needs attention because a premium texture does not automatically provide high environmental resistance.
White BOPP or PP film is a common route for moisture-resistant product labels and packaging that needs a clean opaque white surface.

White BOPP / PP

White BOPP or PP film is a common route for moisture-resistant product labels and packaging that needs a clean opaque white surface. It can work well on bottles, jars, personal-care products, food packaging and many consumer goods. Adhesive choice remains separate from the face film, especially on PE, PP, HDPE or curved containers. A laminate or varnish can be added for surface protection depending on abrasion, moisture and desired finish.
White BOPP or PP film is a common route for moisture-resistant product labels and packaging that needs a clean opaque white surface. It can work well on bottles, jars, personal-care products, food packaging and many consumer goods

Clear Film

Clear BOPP or PET structures are used for transparent packaging and “no-label look” effects. Final clarity depends on more than the film itself: adhesive clarity, container surface, white-ink strategy, print coverage, application quality and trapped air can all affect appearance. Clear labels benefit from testing on the actual bottle or a representative surface. White ink can be used behind selected graphics where opacity is needed while preserving transparent areas elsewhere.
PET is commonly considered for durable labels where dimensional stability, heat resistance, abrasion resistance or industrial service is more demanding than ordinary packaging.

PET Film

PET is commonly considered for durable labels where dimensional stability, heat resistance, abrasion resistance or industrial service is more demanding than ordinary packaging. It can be used for electronics, automotive, equipment, asset identification and durable product labels depending on the adhesive and protective structure. PET should not be marketed as automatically suitable for every high-temperature or chemical application. Exact resistance remains a property of the complete construction and the test conditions.
PE film offers flexibility for squeezable or deformable containers where a more rigid label may lift or crease as the package moves. It can be considered for personal care, household products and selected flexible packaging applications. Print, adhesive, die cutting and liner behavior must still be matched to the structure. PE is a material family rather than one universal product, so thickness, surface treatment and final performance are confirmed through the selected supplier construction.
PE Film

PE film offers flexibility for squeezable or deformable containers where a more rigid label may lift or crease as the package moves. It can be considered for personal care, household products and selected flexible packaging applications. Print, adhesive, die cutting and liner behavior must still be matched to the structure. PE is a material family rather than one universal product, so thickness, surface treatment and final performance are confirmed through the selected supplier construction.

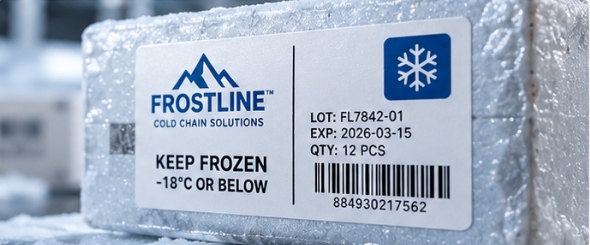
Clear, metallic and holographic films create strong visual effects but also introduce production variables.

Metallic And Holographic Stocks

Metallic and holographic materials provide built-in reflective or diffraction effects before additional printing and finishing are added. They can support premium packaging, promotional labels, security features and high-impact brand decoration. White ink is often used to control where the metallic or holographic background remains visible. The visual effect can change with viewing angle, ink coverage, laminate and lighting, so samples are useful when a brand has a specific appearance target.
Thermal And Specialty Stocks

Thermal And Specialty Stocks

Thermal materials, durable films, low-temperature structures, removable constructions, high-tack options and other specialty stocks are selected according to the project. Special materials may have supplier minimums, longer procurement paths or document requirements that differ from standard paper and film. Philiton keeps common material families within its sourcing and converting system while confirming special performance, certification or brand-specific requirements against the actual material record before they become part of a commercial commitment.

Adhesives, Liners And Components Behind Label Performance

A label is a layered construction. Adhesive, liner, protective coating, foil, tooling and roll hardware can change application performance as much as the printed face material.

Permanent Adhesives

Permanent adhesives are used when the label is expected to remain attached through its intended service life. Selection depends on the substrate, surface energy, curvature, application temperature, service temperature and exposure to moisture, oil or chemicals. A permanent adhesive for glass may not behave the same on PP, PE or HDPE. Philiton therefore requests the actual container material or a representative sample when adhesion risk is high, especially for small-diameter, textured or low-surface-energy applications.

Removable And Repositionable Adhesives

Removable or repositionable constructions are useful for temporary promotions, logistics, reusable containers and applications where clean removal matters. “Removable” is not a permanent guarantee of zero residue under every condition. Dwell time, temperature, surface finish and the adhesive formulation influence how removal changes over time. The required removal window should be defined early, and application testing is recommended when the product surface is sensitive or when residue could create a quality issue.

Release Liners

The liner carries the label through printing, die cutting, rewinding, storage and application. Glassine, film and other liner structures affect stiffness, die-cut control, dispensing and automatic application. Liner choice is particularly important on high-speed roll-label projects because release force and dimensional stability can affect feeding. The liner should be treated as part of the production specification rather than disposable backing with no engineering relevance.

Lamination And Varnish

Lamination and varnish protect printed surfaces and can also change gloss, matte appearance, tactile feel and scanner performance. A laminate may improve abrasion or moisture protection, while a varnish can offer a thinner protective layer or selective visual effect. The choice depends on environment, flexibility, recyclability goals, finishing compatibility and cost. Barcode or QR areas should remain easy to read after the final surface treatment is applied.

Foils And Specialty Layers

Hot foil, cold foil, holographic elements, white ink, scratch-off layers and other specialty components add visual or functional value, but they also create registration, tooling and material interactions that need control. Fine lines, large solid foil areas and embossed foil require different production considerations. Philiton reviews artwork and process compatibility before final tooling or material preparation so decorative intent can be translated into a stable manufacturing route.

Cores, Rolls And Packing Components

Core size, roll diameter, winding direction, splice rules, SKU labels, protective bags, cartons and pallet arrangements affect how labels arrive and run at the destination. A roll label program should specify these details early, especially when labels feed directly into an automatic applicator. Packing components are chosen to protect finished rolls from edge damage, dust, moisture and mix-ups while keeping each SKU identifiable through receiving, storage and production-line use. 

Artwork And Engineering Before The Press Starts

Good print quality starts before printing. Philiton uses artwork, prepress and manufacturing review to convert visual design into controlled production information.

Turn Brand Artwork Into Production-Ready Layers

A design file may look complete on screen and still be incomplete for manufacturing. Philiton reviews the file against the intended label structure before release. Dieline dimensions, bleed, safe area, minimum text size, color separations and image resolution are checked first. Clear and metallic labels can require a separate white-ink layer because the substrate becomes part of the visual design. Foil, spot UV, embossing, debossing, holographic areas and cut paths also need clearly separated production layers rather than being represented only as a visual mockup. Variable data introduces another layer of control. Serial numbers, QR codes, barcodes, data matrix codes or RFID-linked identifiers require a defined data source, print area, sequence rule and verification method. Barcode dimensions and quiet zones should be protected from decorative changes that reduce scan reliability. If several SKUs share one label size, Philiton can review which components can be standardized and which remain unique to each approved artwork. Manufacturing review is designed to raise issues before plates, dies, special materials or production time are committed. Very thin reverse text, tight foil gaps, small internal die-cut corners, excessive ink coverage or an effect placed too close to the cut line can all create unnecessary production risk. The useful output is not simply a prepress PDF. It is an approved production file with dimensions, layers and revision clearly understood by both sides.

Translate Application Conditions Into Label Specifications

Label engineering connects the package and production line to the printed construction. For hand-applied packaging, the discussion may focus on surface material, curvature, cleaning, application temperature and service environment. Automatic application adds roll direction, core diameter, gap, maximum roll diameter, web width and applicator behavior. Industrial labels may add abrasion, heat, oil, chemical exposure or long service life. Security and smart-label programs may add destructibility, VOID behavior, chip/inlay placement, encoding and verification requirements. A common sourcing error is to approve a label based only on a flat sample. A label can look correct and still fail on a small bottle diameter, textured HDPE, oily surface or high-speed applicator. Philiton therefore uses actual containers or representative substrates when application risk justifies testing. For low-surface-energy plastics such as PP, PE or HDPE, adhesive performance may need a higher-tack or specially formulated structure, and contamination or surface treatment can change results even when the plastic name is the same. The engineering output should capture the conditions that matter to production: what surface receives the label, how it is applied, what environment it sees, how long it must remain, what it must resist and how the finished label is delivered. Those inputs give material, adhesive, printing and converting decisions a common technical basis.

Control Versions Before Sampling And Bulk Production

Version control becomes critical when a program has many SKUs, languages, market versions, regulatory statements, serial-number ranges or seasonal graphics. Philiton treats each artwork as a controlled production input even when several SKUs share the same size, material and finish. Shared setup can improve efficiency, but it does not remove the need for separate quantity, artwork approval and QC identification for each design. Before sampling, the file version should be clear enough to avoid testing an outdated design. Before bulk production, approval should lock the artwork revision along with size, material, adhesive, color target, finishing, die cut and relevant roll configuration. Changes after approval can affect prepress, material preparation, tooling or schedule. A change that appears small from a marketing perspective – such as a new foil area, barcode size or container material – can require a technical review because it changes how the job is manufactured or inspected. Repeat orders are also reviewed rather than released blindly. If artwork, material, supplier batch, quantity, finishing, application conditions or compliance requirements have changed, the previous approval may not be sufficient. Keeping the revision and specification connected protects both packaging consistency and production accountability over the life of the program.

Printing Routes Selected By Quantity And Specification

Printing RouteBest FitMain Manufacturing StrengthMain Limitation / Review PointTypical Philiton Use
Digital PrintingSamples, short runs, multi-SKU, launch programs, variable artworkFast version changes and lower setup burden than plate-based methodsUnit economics change as volume grows; special colors and finishing still require reviewLaunch labels, short-run packaging, multiple versions
Flexographic PrintingRepeat roll labels and medium-to-high volume programsEfficient roll production with strong converting integrationPlates/setup and process planning matter more at lower quantityPackaging labels, logistics labels, repeat production
Screen PrintingSelected functional inks, high ink deposit and specialty effectsStrong coverage and distinctive functional or decorative layersNot suitable for every artwork, material or speed targetSpecialty coatings, opaque or functional elements
UV / UV-Related ProcessesPremium graphics and selected specialty applicationsFast curing and compatibility with decorative process combinationsMaterial surface and final effect require process reviewPremium labels, specialty print and decoration
Variable Data PrintingSerial numbers, QR, barcode and unique identifiersEach label can carry controlled unique informationData integrity, sequence control and verification must be definedTraceability, security, logistics and promotional programs
Thermal / Thermal TransferLogistics, warehouse, inventory and secondary printing systemsSupports later on-demand information printingRibbon/material compatibility and service environment affect durabilityShipping, barcode, warehouse and industrial identification

Finishing And Converting Build The Final Label

Printing creates the graphic layer; finishing and converting control protection, texture, decoration, shape, release behavior and the final roll or sheet delivered to production.
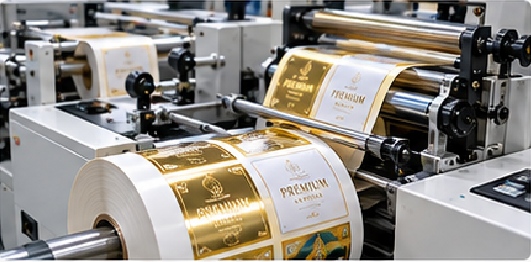
Hot Foil Stamping

Hot Foil Stamping

Hot foil uses heat and pressure to transfer metallic or specialty foil onto selected artwork. It is widely used for wine, spirits, cosmetics, gifts and premium packaging. Fine lines, large solids, small reverse areas and registration with embossing all affect tooling and production stability. Philiton reviews foil artwork before tooling so the decorative target is matched to a manufacturable foil area rather than approved only from a screen rendering.
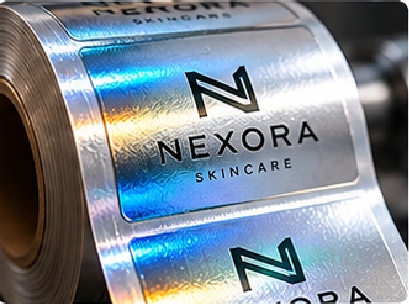
Cold foil is integrated differently from traditional hot stamping and can be suitable for broader metallic graphics or roll-production workflows depending on the design and material.

Cold Foil

Cold foil is integrated differently from traditional hot stamping and can be suitable for broader metallic graphics or roll-production workflows depending on the design and material. The effect can be combined with printed color to create metallic tones beyond standard gold or silver. Choice between hot and cold foil depends on artwork, substrate, run size, equipment route and appearance target. A physical sample is preferable when metallic density or fine registration is important.
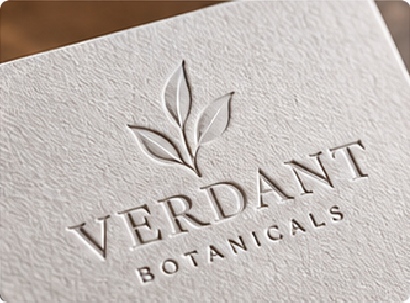
Embossing raises selected areas while debossing presses them inward, adding tactile structure to paper or compatible label materials.

Embossing And Debossing

Embossing raises selected areas while debossing presses them inward, adding tactile structure to paper or compatible label materials. Effects are strongest when artwork, substrate thickness, tooling depth and printed registration are planned together. Very small details or heavy textured materials can change how the relief appears. Premium brand programs often combine embossing with foil, but the process stack should be sampled because each extra registration step increases manufacturing sensitivity.
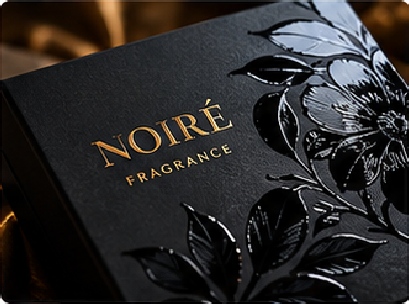
Spot UV creates selective gloss or contrast, while raised UV adds a more pronounced tactile layer.

Spot And Raised UV

Spot UV creates selective gloss or contrast, while raised UV adds a more pronounced tactile layer. These effects can highlight logos, typography or product details without covering the entire label surface. Coating height, edge definition, material compatibility and later die cutting need consideration. The best result comes from planning the effect as a manufacturing layer in the artwork rather than adding it after all other design decisions are already fixed.
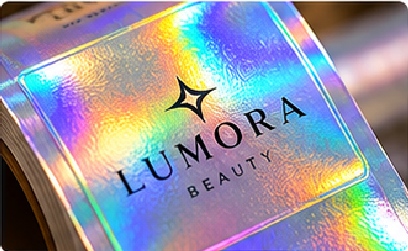
Holographic effects can come from a holographic face stock, transferred element or dedicated security construction.

Holographic Effects

Holographic effects can come from a holographic face stock, transferred element or dedicated security construction. Decorative holography is different from an authentication system, even when both create a similar visual impression. Philiton can combine holographic materials with print, white ink, variable data or tamper-evident structures. Brand-protection projects should define what the feature is expected to prove and how it will be verified before selecting the production route.
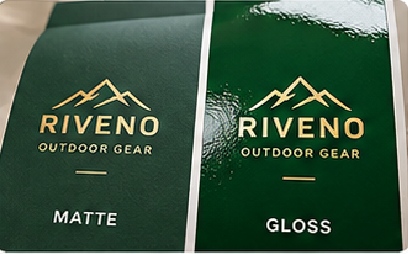
Lamination or protective coating can improve surface resistance, change gloss level, add soft-touch character or protect variable information.

Lamination And Coating

Lamination or protective coating can improve surface resistance, change gloss level, add soft-touch character or protect variable information. The choice needs to remain compatible with bending, dispensing, scanning, recycling goals and other finishing. A matte laminate, for example, may create a premium appearance but should still be checked around barcode or QR areas if low contrast or glare could affect scanning under real lighting.
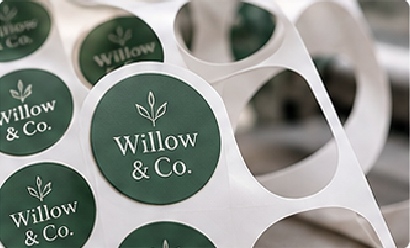
Die cutting creates the final label shape and release edge. Standard rectangles, circles, rounded corners and custom contours all need sufficient liner support and stable waste removal.

Die Cutting And Waste Stripping

Die cutting creates the final label shape and release edge. Standard rectangles, circles, rounded corners and custom contours all need sufficient liner support and stable waste removal. Tight corners, tiny notches and narrow bridges can slow converting or increase waste risk. Philiton reviews shape, size, gap and bleed before tooling so the approved contour can be converted consistently rather than judged only as a digital outline.
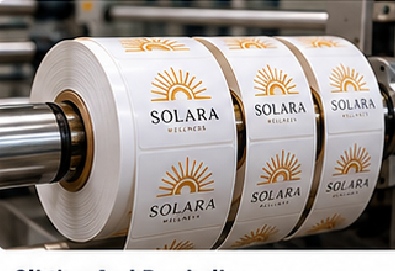
Slitting and rewinding turn the printed web into the final roll configuration required by warehousing, hand application or automated equipment

Slitting And Rewinding

Slitting and rewinding turn the printed web into the final roll configuration required by warehousing, hand application or automated equipment. Web width, core, winding direction, roll diameter, splice policy and SKU separation are controlled at this stage. For automatic application, the final roll specification is part of product functionality. Inspection can be integrated with rewinding so defects are identified or removed before finished rolls are packed.
Sampling, Tooling And Approval Before Bulk Production

Sampling is used to close material, visual, dimensional and functional risk. Tooling or production setup is added only where the specification requires it.
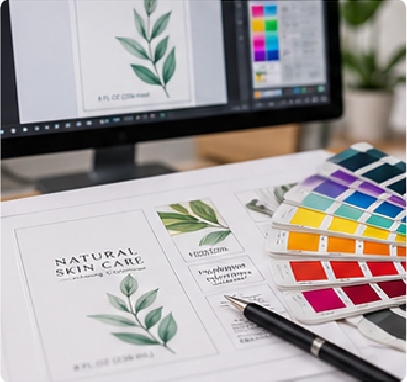
Digital and printed proofs are useful when artwork, layout, color direction or SKU versions need review before a more complex production sample.

Digital And Print Proofs

Digital and printed proofs are useful when artwork, layout, color direction or SKU versions need review before a more complex production sample. They can reduce the cost of discovering file mistakes late in the process. A proof does not automatically reproduce every production effect, especially when bulk manufacture requires dedicated plates, dies, foil tooling, embossing tools or special materials. Known differences should be identified during approval so the proof is used for the correct decision.
Material And Adhesive Samples

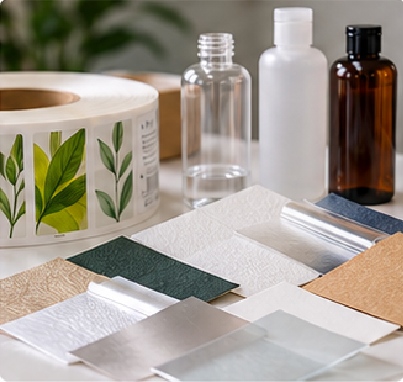
Material And Adhesive Samples

Material sampling is important when clarity, texture, stiffness, adhesion or environmental behavior affects the project. Philiton can prepare or source representative material options for review. Actual containers or substrate samples are especially useful for low-surface-energy plastics, small diameters, freezer, oil, moisture and automatic application conditions. A sample should answer a defined question – for example adhesion to HDPE or appearance of clear film on a transparent bottle – rather than simply provide a generic swatch.
Dies, Plates And Tooling

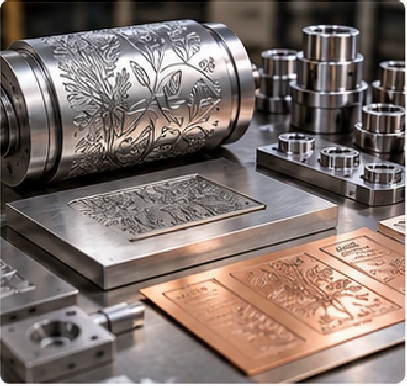
Dies, Plates And Tooling

Some printing and finishing routes require dedicated plates, cutting dies, foil tooling, embossing tools or other setup. Tooling is project-specific, and whether it can be reused depends on process, design stability, condition and storage arrangement. Digital printing may avoid traditional print plates, but die cutting or special finishing can still require tooling. Philiton reviews which setup items are actually needed after size, shape, artwork and finishing are clear, avoiding unnecessary tooling assumptions at the early inquiry stage.
Production Sample Approval

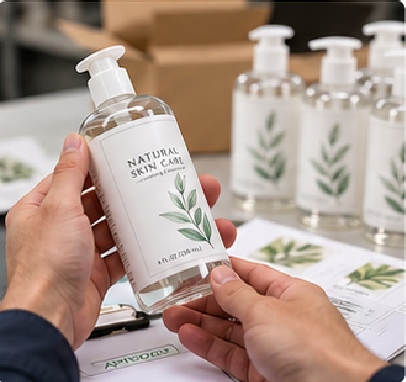
Production Sample Approval

A production-intent sample is used when the final appearance, structure or function needs to be validated close to the planned manufacturing route. Approval should cover the dimensions that matter: artwork revision, size, material, adhesive, color target, white ink, finishing, die cut, roll configuration, barcode/QR or functional requirement where relevant. Sample timing is confirmed by the chosen material and process; complex tooling, special materials, RFID/NFC components or multiple finishing steps can extend preparation compared with a straightforward printed proof. 

Production Details That Protect Repeatability At Scale

Stable label production depends on process control between approved artwork and packed rolls. Philiton organizes production around the specification rather than only the press run.

Control Printing, Registration And Color Through The Run

Production control begins with the approved reference and the correct material lot, artwork revision and process setup. Print color, registration, white ink, variable information and decorative layers are monitored according to the job. Jobs with foil, embossing, spot UV or multiple passes require extra attention because each process adds another registration relationship. The manufacturing objective is not to make the first few labels look correct; it is to keep the agreed appearance and functional elements within a controlled process for the full quantity. Color expectations should be defined before production. A supplied Pantone reference, approved printed sample or measurable color target can provide a clearer standard than a monitor image. Substrate color and transparency also matter: the same ink can appear different on white paper, clear BOPP, metallic film or textured stock. For repeat orders, Philiton can compare the current setup with the approved reference, but material and process changes still need review when they could affect appearance. Variable-data work requires a separate control mindset. Serial ranges, QR content, barcodes and data files must be linked to the correct artwork and SKU. Verification can be included according to the project so missing, duplicated or unreadable information is identified before packing. The exact verification scope should be agreed in advance rather than assumed from the word “variable.”

Control Die Cutting, Matrix Removal And Roll Configuration

A label is not finished when printing stops. Die cutting must create a clean release edge without cutting through the liner, while matrix waste needs to strip reliably around the shape. Small gaps, narrow corners, deep cuts or complex contours can increase converting sensitivity. The die line therefore belongs in the engineering review, especially when a label will be dispensed automatically or when many labels are packed tightly on one roll. After die cutting, slitting and rewinding establish the commercial delivery format. Roll direction, core diameter, web width, maximum roll diameter, labels across, splice arrangement and quantity per roll can all matter to the receiving line. Philiton can separate and identify multiple SKUs so the warehouse or packing line does not need to decode mixed rolls later. When a label is designed for automatic application, the finished roll configuration should be treated as a controlled specification rather than a packing preference. Packing protects those converted rolls from edge damage, dust, moisture and mix-ups during international shipment. Cartons, internal bags, roll labels and SKU identification are organized around the order and destination. Large or repeat programs can also define packing standards that remain consistent across future releases.

Manage Changes Before They Become Production Problems

The biggest production risk is often not a press problem but an uncontrolled change. A revised artwork, different bottle, new adhesive, replacement material, updated barcode, changed roll direction or additional finishing step can alter the manufacturing route after a previous version has already been approved. Philiton therefore reviews repeat and revised jobs against the existing specification rather than assuming the previous setup can always be copied without evaluation. Change control matters more as programs become larger. A small launch run may have one designer and one SKU; a mature program can include regional artwork, seasonal versions, contract packers, multiple warehouses and automatic application equipment. The project record should make it clear which artwork is current, what the approved material and finish are, what changed, and whether a new sample or test is needed. This discipline also protects commercial planning. Material procurement, tooling and production scheduling can begin with greater confidence when the specification is stable. If a late change resets prepress or material preparation, the schedule should be re-evaluated openly rather than hidden inside a fixed lead-time promise. 

Scale From Launch Runs To Repeat Manufacturing

Philiton supports controlled entry quantities and larger repeat programs. Quantity planning is matched to material, SKU structure, tooling, print method and expected reorder pattern.

Around 500-Piece Entry Point

Many standard custom labels and stickers can begin from approximately 500 pieces, subject to material, process, finishing, size and SKU. The value is not simply a small MOQ. It allows a new product, regional version, supplier trial or packaging update to enter production without committing immediately to excessive inventory. Special materials, dedicated holograms, RFID/NFC, special adhesives and complex security constructions may require different minimums because their suppliers or setup processes create higher thresholds.

1,000-5,000 Piece Early Reorders

Early reorder quantities often reveal which SKUs are becoming stable and which artwork or packaging details still change. Similar SKUs can sometimes share compatible materials and production setup, but each design remains separately approved and identified for QC. Philiton can use forecast information to review whether digital production still provides the best balance of setup and flexibility or whether the program is moving toward a more efficient repeat route. These quantity bands are planning references, not fixed pricing rules.

5,000-50,000 Piece Growth Programs

As a program grows, setup cost can be spread across more labels and production efficiency becomes more important. Material planning, roll configuration, pack quantity, inspection and release scheduling also become more structured. Philiton can evaluate whether flexographic or another roll-production route offers better manufacturing economics for the approved specification. The decision is not made by quantity alone; material, color coverage, finishing, SKU count and change frequency can keep digital production attractive for some growing programs.

50,000+ Volume Review

Higher-volume programs justify a broader manufacturing review rather than an automatic price reduction. Forecast, annual demand, call-off frequency, number of SKUs, material availability, tooling reuse, production scheduling and logistics all influence the route. Philiton can review whether the program should use flexographic, hybrid or another suitable workflow, and which specifications should be standardized across SKUs. The objective is a repeatable supply model with controlled changes, not simply the lowest theoretical unit price.

Multi-SKU Production Planning

Multiple SKUs create opportunities and risks. Shared size, material, adhesive and finishing can improve setup efficiency, but each artwork still needs its own approved file, quantity and QC identification. Version differences should be visible in the production plan so similar designs do not become mixed. Philiton can review grouping opportunities without treating total order quantity as a substitute for per-SKU manufacturing requirements. Programs with frequent artwork changes benefit from clear forecast and release planning.

Repeat Order Management

Repeat orders can be more efficient when artwork, material, adhesive, tooling and production parameters remain unchanged and materials are available. They still require order review and QC. Philiton checks whether artwork, quantity, finish, delivery or application conditions have changed before release. This protects the approved standard while allowing stable programs to move through manufacturing with less redevelopment than a first-time job.
Quality Control From Material Receipt To Final Release

Inspection is built around project risk. Philiton combines incoming checks, process controls, final inspection, vision inspection and application testing where the specification requires them.
Incoming Material Control

Incoming Material Control

Base papers, films, adhesives, foils, liners and specialty materials are sourced externally, so incoming material control is a critical first step. Identification, quantity, appearance and project-relevant documentation should match the purchase and production requirements before the material enters the job. Supplier certificates or test reports are kept distinct from finished-product verification. A material report does not automatically prove how the converted label will perform on a specific bottle, temperature or chemical environment.
Artwork And Prepress Check

Artwork And Prepress Check

The approved artwork version, dieline, dimensions, colors, white ink, finishing layers, barcode areas and variable-data fields are checked before production release. This step helps prevent a correct press setup from printing the wrong revision. Multi-SKU and regulated-information programs benefit from clear artwork identification because similar graphics can hide important differences in ingredients, language, serial ranges or product codes. Production should begin from a controlled file rather than an email attachment whose revision is unclear.
Print Process Inspection

Print Process Inspection

During printing, operators and quality personnel monitor the characteristics relevant to the job: color, registration, contamination, missing print, white ink, variable information and surface appearance. The exact control method depends on the print technology and approved standard. Decorative processes add their own checkpoints because foil, embossing, UV or multiple passes must remain aligned with the printed graphics and die line. Problems are easier to control during the run than after the full quantity has been converted.
Die Cut And Converting Check

Die Cut And Converting Check

Die cutting is checked for shape, position, clean release and liner integrity. Matrix stripping, slitting, rewind direction, core and roll diameter are reviewed according to the delivery specification. Automatic application projects require particular attention because a small configuration error can create stoppages even when the printed label itself is visually acceptable. Finished rolls should remain clearly identified by SKU and quantity through packing.
100% Vision Inspection

100% Vision Inspection

Philiton has automated vision-inspection capability for applicable roll-label projects. The system can be used to identify print defects, stains, missing print, registration problems, die-cut or waste-stripping issues, barcode/QR problems and selected variable-data defects, depending on the project setup. “100% inspection” refers to the capability to inspect the web or finished roll through a vision process; it does not mean every performance property of every label is destructively tested one by one.
Barcode And Data Verification

Barcode And Data Verification

Machine-readable information needs a defined verification scope. Barcode or QR checks can review print clarity and readability, while variable-data projects may also require sequence or database matching. A scanner passing one sample does not prove the full data set is correct, so the project should state what needs to be verified and at what stage. RFID/NFC work adds encoding and functional read checks according to the selected inlay and data requirements.
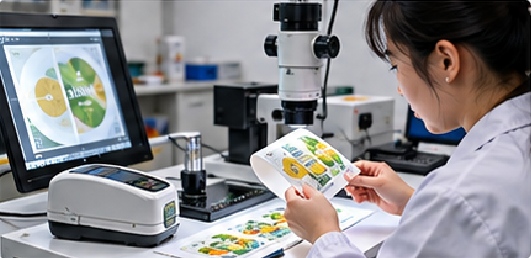
Laboratory And Application Testing

Laboratory And Application Testing

Philiton has in-house testing capability for label projects, including color, adhesive/application, durability and barcode or RFID-related checks where relevant. Exact standards, conditions and acceptance criteria are confirmed by project. Temperature, water, oil, chemical or outdoor claims should never be generalized from a material name alone. The strongest verification uses the intended construction on the actual container or a representative substrate under conditions that reflect real use.
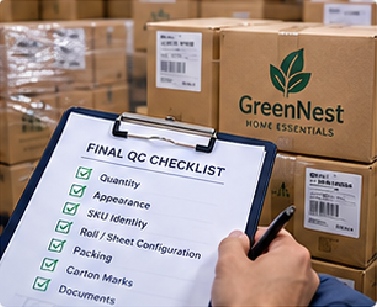
Final QC And Release

Final QC And Release

Final release checks connect the manufactured product back to the order specification. Quantity, appearance, SKU identity, roll or sheet configuration, packing, carton marks and required records are reviewed before shipment. Where inspection reports, packing lists or other agreed documents are required, they should correspond to the released batch. The purpose is a traceable handover from manufacturing to logistics rather than a final visual glance after production has already been packed. 
Security, Variable Data, RFID And NFC Manufacturing

Philiton supports security and smart-label programs where printed graphics, controlled data, converting and verification must work together in one production route.

Variable Data Labels

Variable data can include serial numbers, batch information, QR codes, barcodes, data matrix codes or unique promotional identifiers. The project should define source data, sequence rules, artwork position, duplication tolerance and verification method before production. Philiton can combine variable printing with roll conversion and inspection so the unique information remains connected to the correct label and SKU. Database ownership and downstream systems remain governed by the project agreement.

Tamper-Evident Structures

Tamper-evident labels use a physical response to opening or removal. VOID transfer, destructible film, eggshell-type constructions, security seals and other structures behave differently, so the program should define the required evidence of tampering. Substrate material, surface texture and application conditions can change performance. Philiton can print and convert these structures with serial or security graphics, while the exact material behavior should be validated on the intended package.

Holographic Security

Holographic materials can provide visual complexity and brand differentiation, but a hologram alone does not automatically create a complete authentication system. Philiton can combine holographic stocks or elements with printed information, unique codes or tamper-evident structures. Programs requiring proprietary holograms, dedicated masters or specific security features need separate project sourcing and tooling review. The verification method should be defined alongside the visual design.

RFID Labels

RFID labels combine printed construction with an inlay and encoded data. Philiton supports printing, converting, encoding and functional verification for suitable UHF and HF projects. Chip brand, inlay model, frequency, read range and antenna behavior must be selected for the actual use case. Packaging materials, nearby metal or liquid and tag orientation can affect performance, so functional testing should reflect the intended environment rather than relying on a generic read-distance claim.

NFC Labels

NFC labels can support product authentication, brand interaction, information access and smart packaging. The physical label, memory requirements, encoding content, locking rules and verification process should be established before bulk production. Philiton can integrate printing, converting and encoding around the selected NFC inlay. Website, app, cloud or other external data-platform responsibilities are separated from the physical label manufacturing scope unless specifically included in the project.

Data And Confidentiality Control

Security projects often involve sensitive artwork, unreleased products, unique codes, RFID data and commercial information. Philiton can work under NDA and project-specific access rules, keeping customer designs and data restricted to the manufacturing purpose. Unique identifiers should not be reused across unrelated jobs. Disposal, revision and file-handling requirements can be defined when the program requires stronger controls than a normal packaging label order.

Factory Floor, Equipment And Team Behind Production

Manufacturing evidence should connect people and equipment to actual process steps. Philiton focuses on verifiable capability categories instead of unsupported machine-count or speed claims.
Artwork And Prepress Area

Artwork And Prepress Area

Artwork workstations and prepress capability support dielines, separations, production layers, variable-data setup and job preparation before printing. The value is early control of revision and manufacturability, especially for clear labels, foil, embossing, barcode or multi-SKU programs. A strong prepress stage reduces the chance that a press operator has to solve a design-file problem after material and machine time have already been committed.
Digital Printing Area

Digital Printing Area

Digital label printing supports samples, shorter runs, multiple SKUs, fast design changes and variable-data work without traditional printing plates. It is an important part of Philiton’s flexible manufacturing model because launch programs can start at manageable quantities while maintaining access to downstream finishing, die cutting, inspection and packing. Digital is selected where it fits the job; larger repeat programs can be reviewed for other routes as economics and specification stability change.
Flexographic Production

Flexographic Production

Flexographic capability supports repeat roll-label production where efficiency, roll handling and inline converting are important. Plate preparation and setup make the production logic different from digital, so quantity, SKU count, color, material and finishing determine whether flexo is the better route. Philiton uses flexographic capability as part of a broader manufacturing system rather than presenting it as a universal answer for every label.

Finishing And Converting

Foil, embossing/debossing, lamination, holographic processing, die cutting, waste removal, slitting and rewinding create the finished commercial format after print. These processes are where a flat printed web becomes a functional roll, sheet or individual label. Complex projects often need several operations in sequence, so registration, tooling and material behavior are managed across the full route rather than evaluated one process at a time.
Inspection And Testing

Inspection And Testing

Automatic vision-inspection equipment and in-house testing capability support print, die-cut, code and application verification. Quality work is connected to the job specification: not every label needs the same test, and destructive testing is handled by agreed sampling rather than by unrealistic claims of testing every unit. Inspection records, sample references and project criteria give quality teams a more useful basis for approval than general “high quality” language.
Skilled Manufacturing Team

Skilled Manufacturing Team

Philiton has more than 200 employees, including 91 technical, skilled production and quality personnel combined. These people support process execution, equipment operation, finishing, inspection, testing and quality release. The combined figure is used because separate headcounts by function have not been formalized for public claims. For sourcing teams, the relevant evidence is how those roles participate in engineering review, controlled production and problem resolution through the life of a program. 

Packaging And Delivery Formats For Production Use

Delivery / Packing FormatBest FitKey Specifications To ConfirmPhiliton Manufacturing Consideration
Roll LabelsHand or automatic applicationRoll direction, core, gap, web width, maximum roll diameter, labels per rollSlitting, rewinding, inspection and SKU identification are controlled to the approved configuration
Sheet LabelsManual application, kits, retail packs, small batchesSheet size, labels per sheet, kiss cut, margins and packing quantityDie cutting and sheet handling are planned to prevent edge damage or mixed designs
Individual StickersPromotions, inserts, giveaways, retail distributionDie cut / kiss cut style, liner size, count per bag or cartonPacking method is selected for easy counting and distribution
Fan-Fold LabelsThermal and logistics workflowsFold pitch, stack size, material and printer compatibilityProduction route is matched to later thermal or transfer printing requirements
Multi-SKU PackingPrograms with many variantsSKU code, quantity, carton separation, labels per roll/sheetEach approved artwork remains separately identified through QC and packing
Neutral / Blind-Shipment PackingDistributors, brokers and channel programsBranding on cartons/documents, consignee, return informationCommercial terms and confidentiality requirements are confirmed per project
Export Cartons / PalletsInternational bulk shipmentCarton count, gross/net weight, dimensions, palletization where requiredPacking list and shipment records correspond to released finished goods
Courier / Air / Sea ShippingSamples through bulk productionDestination, postal code/port, urgency, volume, IncotermTransit time and freight are quoted by current route; no single fixed global delivery time is applied

Compliance And Documentation Managed By Project Scope

Philiton separates manufacturing responsibility from legal-market responsibility. Documents, material evidence and testing are matched to the actual label, market and contractual requirement.

Material Documentation

Material documentation can include supplier technical information, certificates, COA or test reports when available and relevant to the selected construction. A raw-material document applies to the material and scope stated on it; it should not be expanded into a universal claim for every finished label. Special certification requirements should be identified during material selection so Philiton can verify the correct supplier construction before quotation or production approval.

Project-Specific Testing

Adhesion, temperature, water, oil, chemical, abrasion, barcode or RFID performance depends on the final construction and test conditions. Philiton can perform relevant internal checks and coordinate third-party testing when a program requires external evidence. The required method, acceptance criteria and responsibility should be agreed before testing. A report from one material or one test condition is not presented as proof for unrelated products or environments.

Artwork And Regulatory Content

Philiton manufactures the approved artwork but does not replace the brand owner, importer or other legal party responsible for market-specific mandatory content. Ingredient statements, warnings, language, nutrition, medical claims, product registration or other legal text should be supplied and approved by the responsible organization. Philiton’s role is to control the approved version and reproduce it correctly through the agreed print and variable-data process.

Traceability And Production Records

Approved artwork, material identification, production information, inspection outputs, packing and shipment records can support project traceability. The exact record set depends on product risk and commercial requirements. Enterprise programs can define additional document expectations during supplier qualification. Philiton avoids claiming a universal traceability package for every order; the useful approach is to agree which records matter before production so the released batch can be linked to the approved specification.

Audit And Supplier Review

Factory visits, audits, sample reviews and supplier-qualification requests can be supported when the project reaches the appropriate stage. Public information confirms manufacturing operations in Shenzhen and Dongguan, while specific site details can be provided for legitimate audit or commercial needs. Audit scope should match the project: a packaging label program, security-label program and RFID project may require different manufacturing, data or document reviews.

Export Documentation

Philiton can provide commercial invoices and packing lists for international shipments and can support origin or customs information according to destination requirements. HS-code classification and import responsibility depend on the product, Incoterm and destination rules, so final import treatment remains subject to the importer and customs process. Shipping documents are prepared against actual order and packing information rather than generic templates detached from the shipment.

Representative Manufacturing Cases Across Three Markets

The examples below are representative project scenarios built from Philiton’s documented manufacturing scope. They illustrate production logic and do not identify named client records.
United States Skincare Launch

United States Skincare Launch

A U.S. skincare brand prepared six products in two bottle sizes and needed 18,000 labels across 12 artworks for an initial retail and e-commerce launch. The program used clear and white film structures, white ink, matte surface protection and gold foil on selected front labels. Philiton’s workflow would start by separating the 12 artwork revisions, testing clarity and adhesion on the supplied PET and HDPE bottles, then approving roll direction and core for the contract packer’s applicator. Production would combine compatible materials where possible while keeping each SKU independently identified through inspection and packing. Forecast information would be used to review a more efficient repeat route after the launch quantities stabilize.
Germany Industrial Equipment Program

Germany Industrial Equipment Program

A German industrial equipment company required 25,000 durable labels across four component families, including serial numbers, QR codes and warning information. The representative construction would use a durable film with project-selected adhesive and protective surface layer, with testing focused on the actual metal and coated surfaces rather than a generic “industrial” claim. Philiton would review the data file, code size, variable sequence, die-cut dimensions and roll configuration before a production sample. During manufacture, variable-data verification, print inspection, die-cut control and SKU separation would be defined as release points. Repeat orders would retain the approved artwork and material reference unless the equipment surface, data format or environmental requirement changes.
Australia Beverage Multi-SKU Rollout

Australia Beverage Multi-SKU Rollout

An Australian beverage group planned 36,000 pressure-sensitive labels for six flavors across chilled glass and PET bottles. The representative program would compare white BOPP and clear-film options, evaluate condensation and bottle curvature, and use foil or selective UV only where the decoration remained compatible with the chosen substrate. Each flavor would have its own approved artwork, quantity and carton identification, while common roll specifications could simplify application at the filling partner. Philiton would use a production-intent sample to confirm color, material, finish and roll direction before bulk release. Freight would then be quoted against final carton volume, destination and required delivery window rather than using a fixed global transit promise.

Frequently Asked Questions About Label Factory Manufacturing

Philiton is a custom label, sticker, tag and specialty-printing manufacturer with manufacturing operations in Shenzhen and Dongguan. Core work covers artwork/prepress, printing, finishing, converting, inspection, testing, packing and production management. Base label stocks, papers, films, adhesives, foils and specialty materials are sourced from external suppliers rather than manufactured by Philiton.
Many standard custom label and sticker projects can start from approximately 500 pieces. The workable MOQ depends on material, size, number of SKUs, printing method, finishing, tooling and supplier minimums. Special materials, custom holograms, RFID/NFC inlays, dedicated dies or unusual adhesive structures can require higher project-specific quantities.
Yes. Sampling can confirm size, material, adhesive behavior, print appearance, finishing, die cut, roll configuration and application performance. The most suitable sample route depends on what needs to be approved. A simple print proof, material sample and production-intent sample are not the same. Sample timing is confirmed after material, tooling and process requirements are known.
Yes, when materials, adhesive, finishing and technical specifications are compatible. Similar SKUs can share parts of the production setup, but each design still needs its own approved artwork, quantity and QC identification. Total order quantity does not automatically replace per-SKU requirements, especially when artwork, special finishing or data differ.
Philiton’s manufacturing system includes digital, flexographic, screen, UV-related, variable-data and other label printing capabilities. The route is selected according to material, quantity, color target, SKU structure, finishing and delivery format. Digital and flexographic printing are complementary rather than competing choices; different stages of the same product program may use different routes.
Yes. Automatic-application projects should include roll direction, core diameter, gap, web width, maximum roll diameter and applicator information. The label material and release liner also influence dispensing. Providing the applicator specification early allows printing, die cutting, slitting and rewinding to be planned around the line rather than correcting roll configuration after production.
Philiton has automated vision-inspection capability for applicable roll-label projects. It can be used to identify print defects, registration issues, die-cut or waste-stripping problems, barcode/QR defects and selected variable-data problems depending on setup. It does not mean every property of every label receives 100% destructive testing; performance testing follows an agreed method and sampling plan.
Yes. Philiton supports printing, converting, encoding and functional verification for suitable RFID and NFC label programs. Chip brand, inlay model, frequency, read range, memory, encoding and system integration are confirmed by project because they depend on application and selected components. Philiton does not present every RFID chip or inlay as internally manufactured.
Normally provide label size, shape, quantity, number of SKUs, application surface, material if known, artwork, printing requirements, finishing, roll/sheet/individual format, roll direction and core if applicable, packing needs and delivery destination. Environment, automatic application, security or RFID requirements should also be included when relevant because they can change material and process selection.
Repeat orders are reviewed against the approved artwork, material, adhesive, tooling and production specification. When those inputs remain unchanged and materials are available, preparation can usually be more efficient than first-time development. If artwork, material, quantity, finishing, packaging or application conditions change, Philiton reviews whether a new proof, sample or technical approval is needed.

Send Your Label Program For Manufacturing Review

A useful quotation starts with enough information to choose the right material, print route, finishing and delivery format. Send the project as it exists today; Philiton can identify which details still need to be confirmed before sampling or production.

Please include:

  • Label size and shape
  • Quantity and number of SKUs
  • Artwork or a reference file
  • Product, container or application surface
  • Material preference, if already specified
  • Printing colors, white ink, foil, embossing, UV or other finishing
  • Roll, sheet or individual delivery format
  • Roll direction, core and applicator details for automatic application
  • Barcode, QR, variable data, security, RFID or NFC requirements
  • Destination and required receipt window

Philiton will review the manufacturing route, material and adhesive considerations, sampling needs, tooling requirements and the information required for a formal quotation. Projects using special materials, compliance documents or functional testing will be identified early so the approval path is clear before bulk production begins.

Get In Touch

  • Our team will answer your inquiries within 12 hours.

  • Your information will be kept strictly confidential.

Get a Fast Quote for Custom Labels & Stickers

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”. 
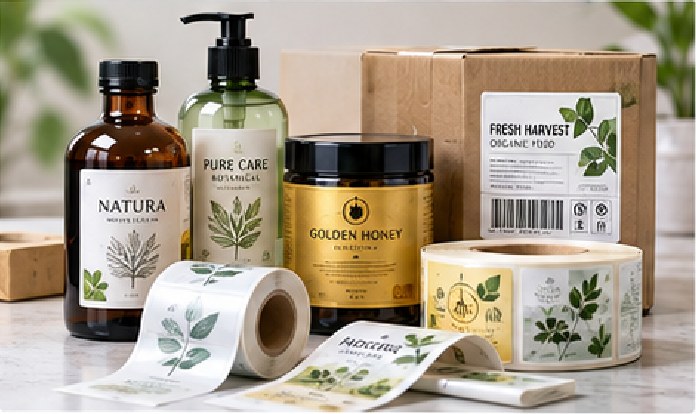
For all inquiries, please feel free to reach out at:

Ask For A Quick Quote

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”. 

For all inquiries, please feel free to reach out at:

Get a Quote Today!

We will contact you within 24 Hours, please pay attention to the email with the suffix“@philiton.com”.